Unwind Ratio
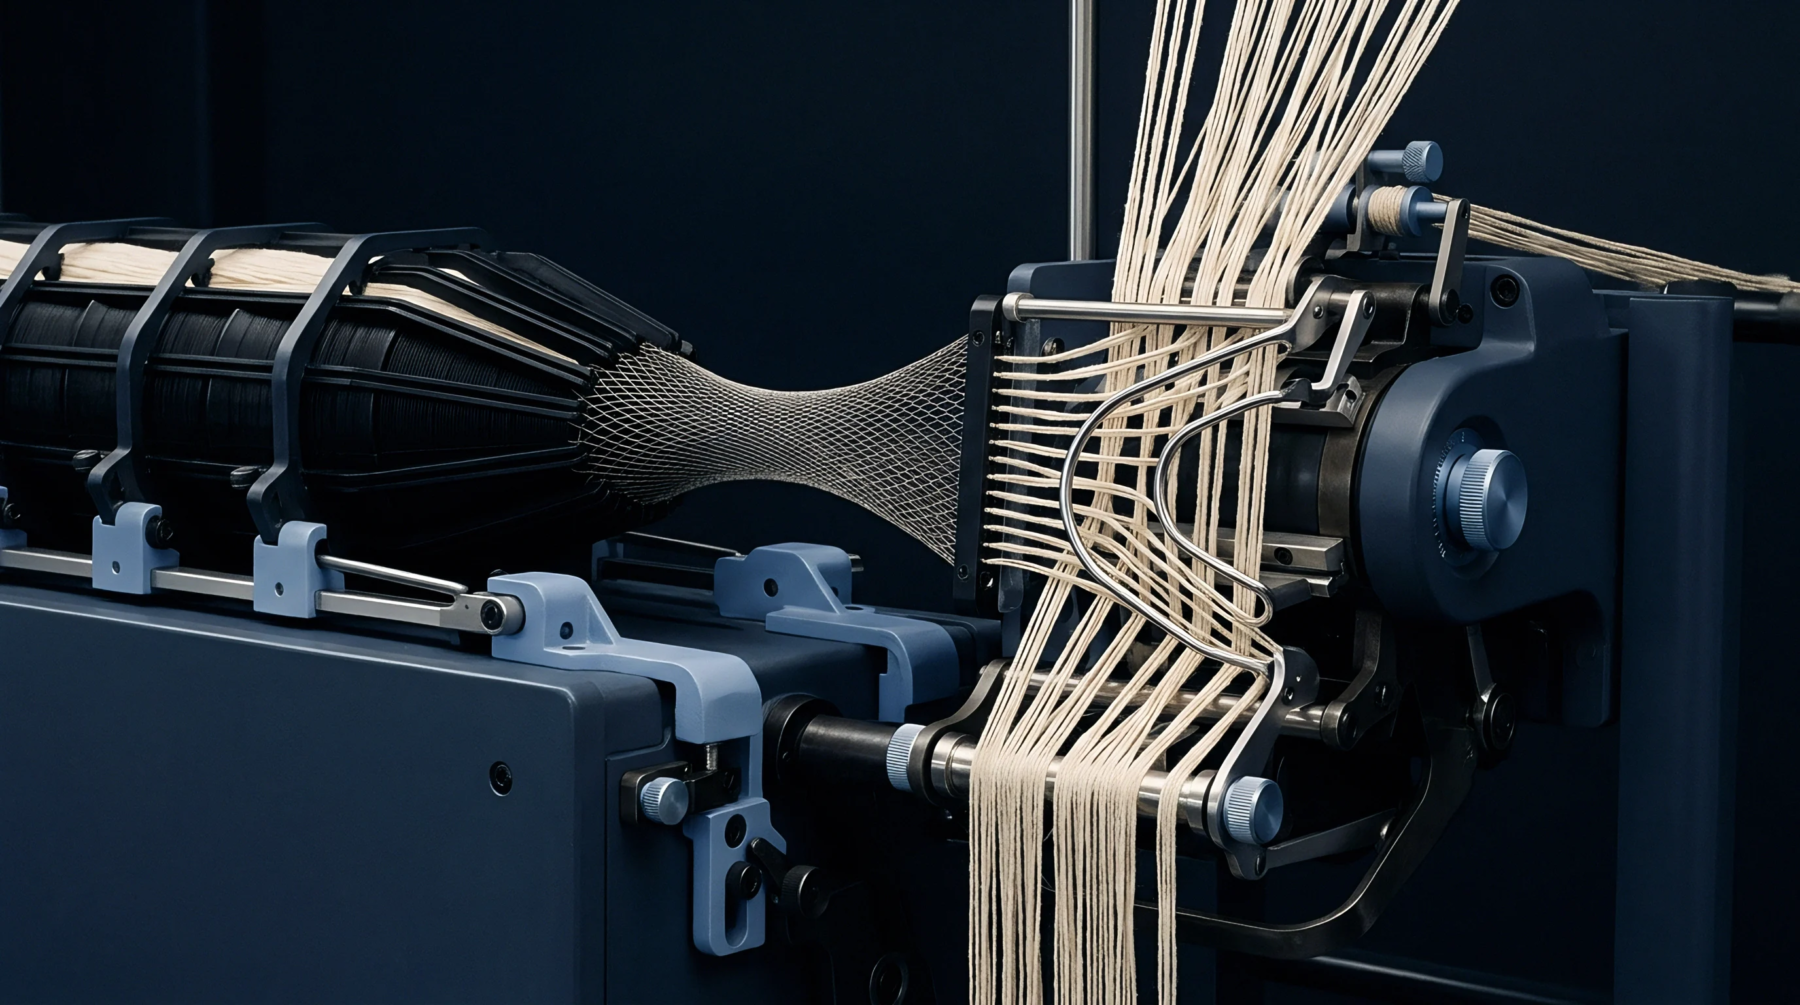
Yarn tension control mechanisms in warping and beaming frames establish the linear draft ratio applied to yarn ends as they leave package spools. The creel unwind draw measures the speed differential between the package delivery surface and the downstream draw roller assembly. Excessive draft at this stage overstretches synthetic filaments, whereas insufficient draft causes yarn sagging and entanglement.
Draft Mechanism
Unwinding yarn packages rotate against mechanical or electronic friction units that regulate individual end delivery. When the downstream collector drum pulls yarn faster than the spool releases, creel unwind draw imposes structural elongation on the filament core. Consistent tension across all creel positions prevents yarn cross-over on the warping beam.
Quality Consequence
Irregular drafting during beam preparation alters linear yarn density and creates shade variation after fabric dyeing. Variations in creel unwind draw introduce differential latent shrinkage across the warp sheet, which shows as corrugated banding in finished goods. Quality inspections at the warper verify draft uniformity across all active spools.
Operating Boundary
Warping speeds above eight hundred meters per minute require automated tension compensating units to maintain stable unwinding conditions. Beyond critical yarn strain limits, creel unwind draw generates filament breakage rather than controlled elongation.