Geometrical Geometry
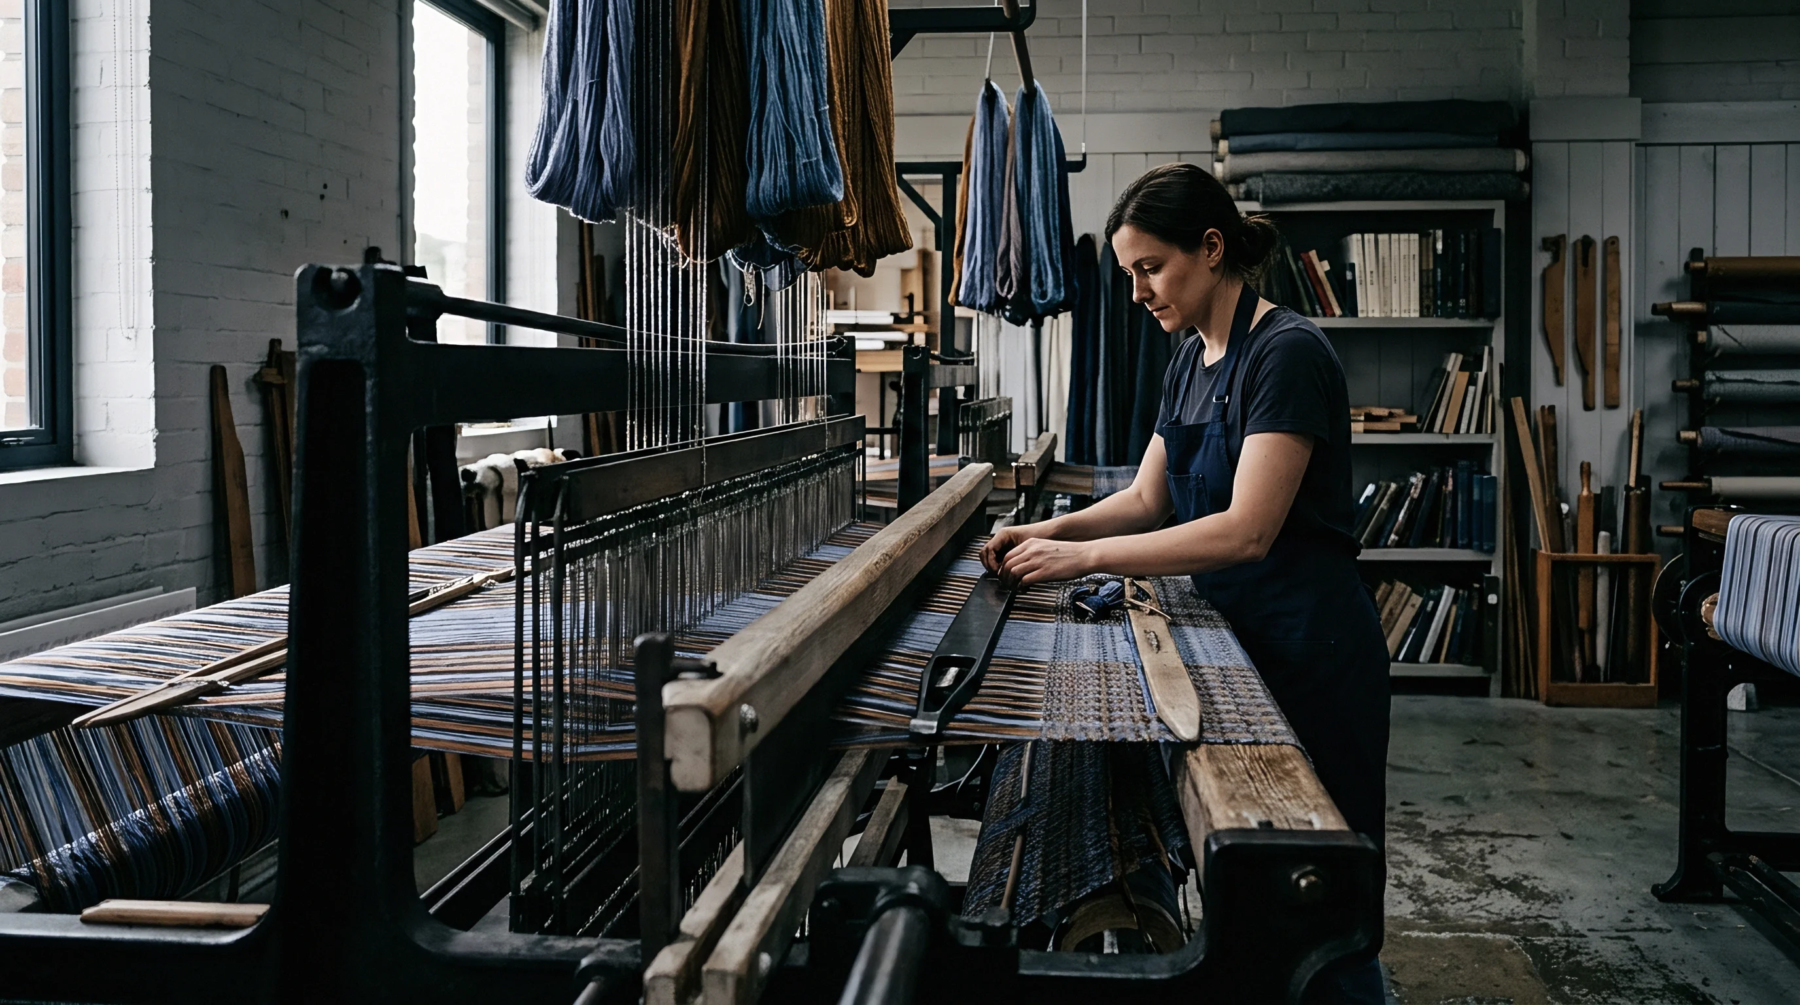
Dynamic separation of warp sheets into upper and lower planes forms a clear channel for weft insertion mechanisms across the loom width. The shed opening represents the vertical gap and angle defined by the divergent yarns between the harness frame heddle eyes and the cloth fell line. It governs the spatial path available to the picking element, functioning exclusively between the initial harness division and the ultimate shed closure during beat-up.
Kinematic Motion
Harness motion profiles dictate the maximum lift height, dwell angle, and timing of cross-over relative to loom crankshaft degrees. Sufficient vertical clearance allows rapier heads, projectile carriers, or air jets to pass through cleanly without catching divergent warp ends. Excessive opening dimensions increase cyclic elongation strain on the warp yarns, accelerating yarn fatigue and shedding rates.
Asymmetric shed settings adjust warp tension balance between upper and lower sheets, improving face fabric appearance in dense constructions.
Tension Limits
Mill settings are calibrated using angle measurement gauges, timing dials, and electronic tension sensors mounted across warp sections. An inadequate shed opening induces weft collision, broken filaments, trailing picks, and mispicks along the outer fabric selvedges. Sizing film flexibility dictates how wide the shed can separate without inducing tensile yarn rupture.
High warp densities demand clean shedding to prevent neighboring fibers from clinging together across adjacent harness frames.
Processing Reliability
Unclean shedding from yarn hairiness causes warp ends to entangle across the neutral axis, creating small loops and fabric defects. Controlling shed geometry minimizes fatigue degradation, balancing clear weft insertion paths against peak mechanical tension on individual ends. Optimizing lift dynamics guarantees high production speeds without compromising woven fabric face quality.