Thermal Stabilization
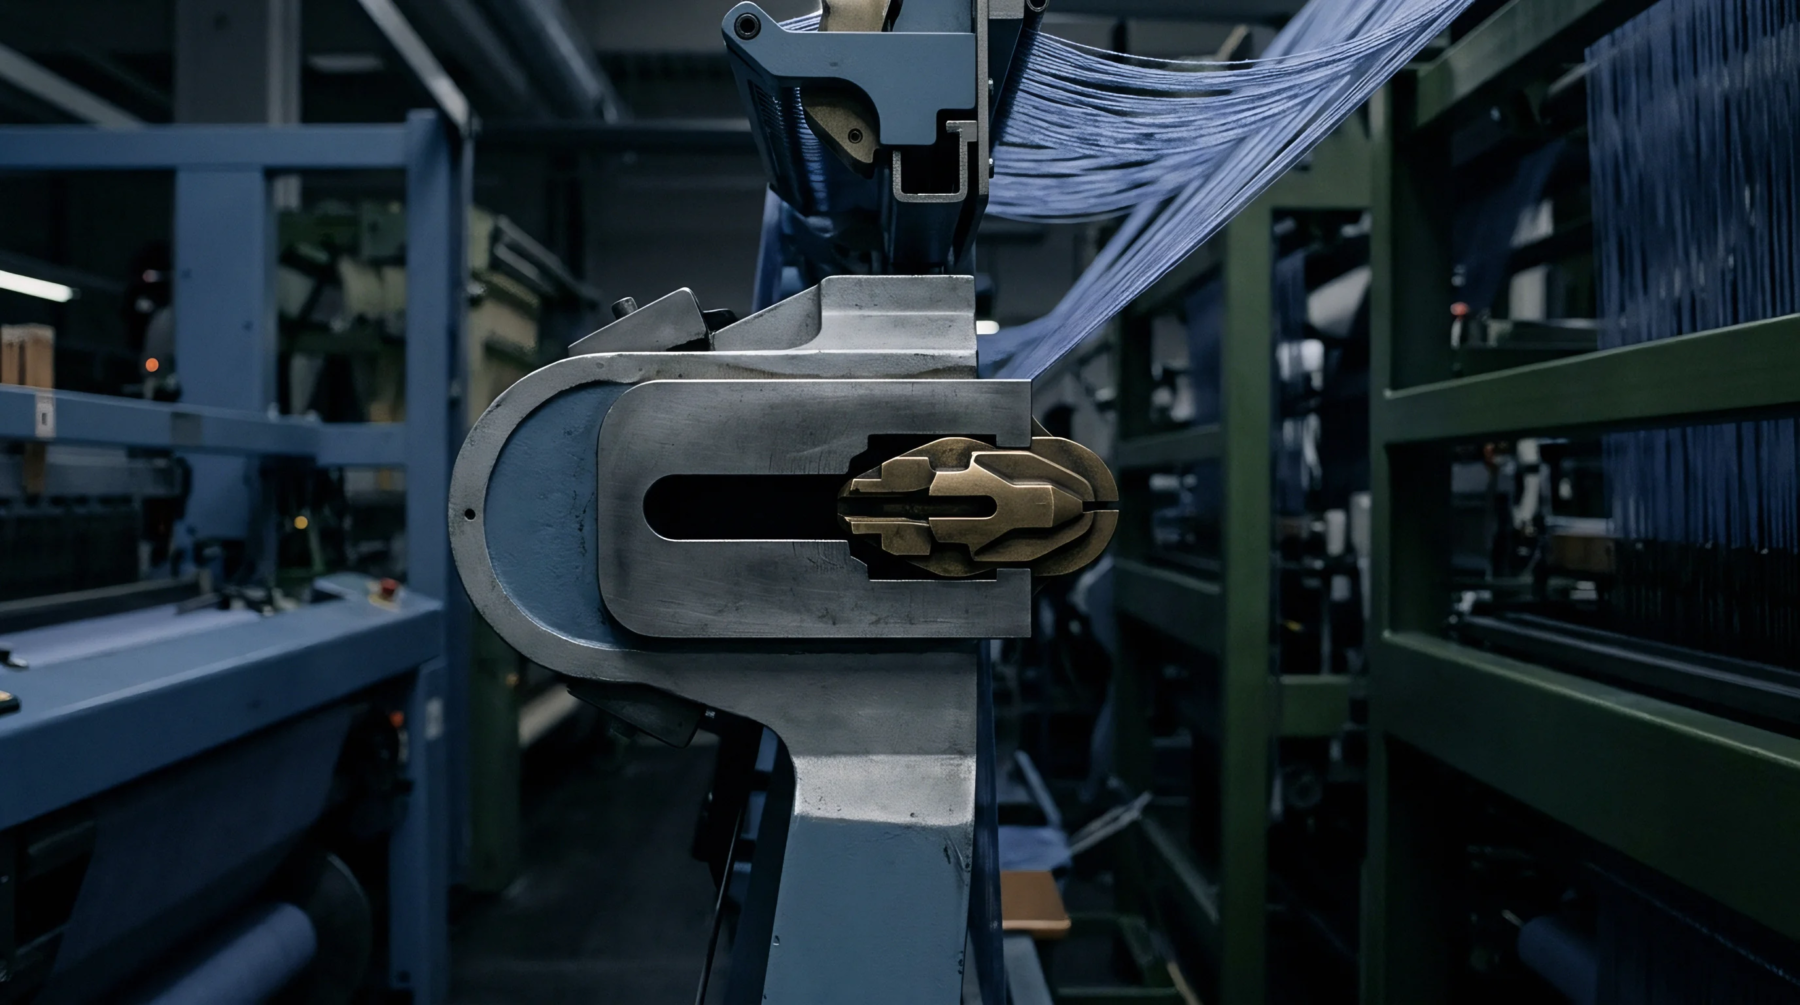
Polyester and polyurethane block copolymers undergo elastane heat setting during continuous tentering in finishing plants to lock molecular orientation. Commercial buyers verify this dimensional recovery parameter through shrinkage testing after wet relaxation cycles. The procedure operates by fixing molecular segments inside a controlled hot air chamber after mechanical stretching.
Tension must remain constant across the entire web to prevent width distortion before cooling begins. Operating temperatures exceed standard drying thresholds to allow polymer chains to reorganize into stable crystalline structures. Boundary conditions restrict the process when excessive dwell time causes yellowing or thermal degradation of the underlying filaments.
Dimensional Recovery
Garment manufacturers depend on elastane heat setting to prevent residual shrinkage during subsequent garment washing and consumer use. Longitudinal relaxation forces act upon the core filament while transverse frames maintain precise fabric width specifications. Excess heat causes polymer cross-linking failures that permanently reduce elastic recovery rates during laundering.
Tension adjustments during processing dictate whether finished jersey knit goods curl along cut edges or remain flat. Laboratory technicians measure recovery percentages using standardized elongation cycles after subjecting samples to high temperature immersion. Production lots failing recovery thresholds return to the mill because dimensional changes exceed acceptable tolerances for cut and sew operations.
Crystalline Formation
Polymer segments reorganize into ordered domains during elastane heat setting when thermal energy exceeds glass transition boundaries. Soft segments remain amorphous while hard segments form hydrogen bonded domains that act as physical cross-links. Molecular orientation achieved during spinning relaxes partially inside the heating zone unless appropriate overfeed values counteract shrinkage.
Cooling jets freeze the newly formed crystalline arrangement before the fabric encounters wind up tensioners. Inadequate dwell time leaves internal stresses unresolved, which triggers spontaneous relaxation later during apparel manufacturing.
Tenter Control
Finishing supervisors monitor dwell time and chain rail width continuously during elastane heat setting to maintain uniform weight per square metre. Temperature sensors positioned inside each drying zone regulate gas burner output to compensate for speed variations. Heat transfer efficiency depends on nozzle design and air velocity across both fabric faces within the convection chamber.
Operators adjust overfeed rollers to introduce positive fullness into the web before the pins engage the selvage edges. Measurement instruments record residual shrinkage values on audit samples taken from the trailing end of every master roll.