Planar Printing
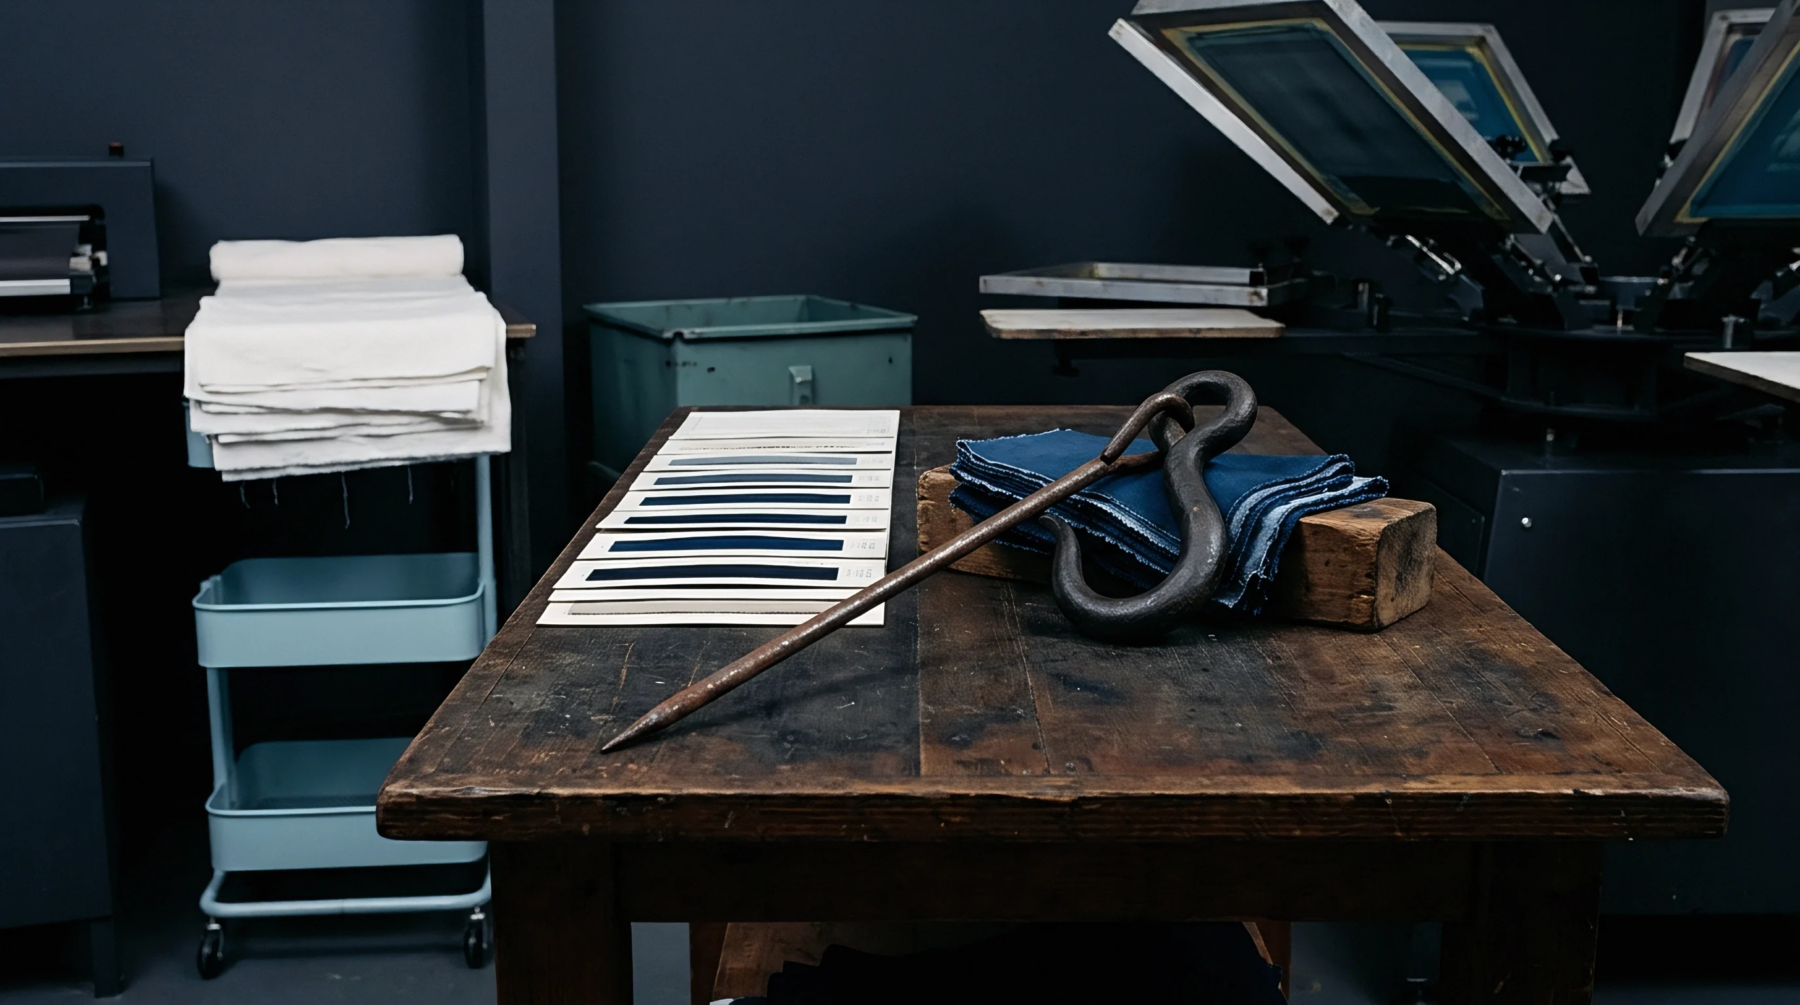
Mechanized surface coloration deposits formulated print pastes across planar fabric substrates through woven mesh screens mounted in rigid rectangular frames. Production facilities operate flatbed screen printing by securing fabric onto an endless moving blanket that indexes forward in precise pitch increments beneath stationary printing stations. Squeegee blades sweep across the open mesh areas of the tensioned screen, forcing paste through image apertures onto the flattened textile beneath.
Each screen frame corresponds to an independent color separation within the overall graphic design. Automated registration pins align individual frames to prevent pattern distortion across wide fabric widths.
Mechanical Application
Precise fabric tension control and continuous table adhesion maintain design alignment during sequential color deposits. Thermoplastic adhesives coated on the conveyor blanket anchor the fabric flat, neutralizing mechanical distortion from squeegee pressure. Squeegee angle, downward pressure, and traverse speed govern print paste volume transfer into the fabric structure.
High screen mesh counts yield fine visual line definition, while lower mesh counts deliver heavier paste loads required for heavy pile fabrics or deep shades. Following the final screen strike, fabric separates from the printing blanket and feeds into continuous hot-air drying ovens.
Pattern Evaluation
Print quality checkpoints evaluate design registration tolerance, paste penetration depth, and color yield against master pattern strikes. Commercial buyers inspect output under standard light cabinets to identify squeegee drag lines, screen clogging faults, and misregistration down the fabric salvage edges. Performance validation includes crocking resistance via AATCC Test Method 8 and wet washfastness via ISO 105-C06 to verify pigment binder curing or dyestuff fixation.
Variations in squeegee durometer hardness or uneven pneumatic pressure cause cross-width shade variations that result in garment piece rejection during cutting room operations.
Substrate Boundaries
Rotary screen units and digital inkjet printers operate continuously rather than through incremental bed indexing, functioning outside the mechanical limits of flatbed tables. The planar frame process cannot handle continuous repeat lengths beyond the physical dimensions of the rectangular screen frame. Extremely lightweight sheer fabrics or high-stretch knits present handling difficulties if adhesive blanket release forces distort the warp and weft alignments.
Production speeds remain mechanically capped by the start-and-stop indexing sequence, running substantially slower than continuous rotary cylinder printing. Paste viscosity thresholds limit color delivery, as excessively fluid pastes bleed past stencil borders, while heavy pastes fail to clear mesh apertures.