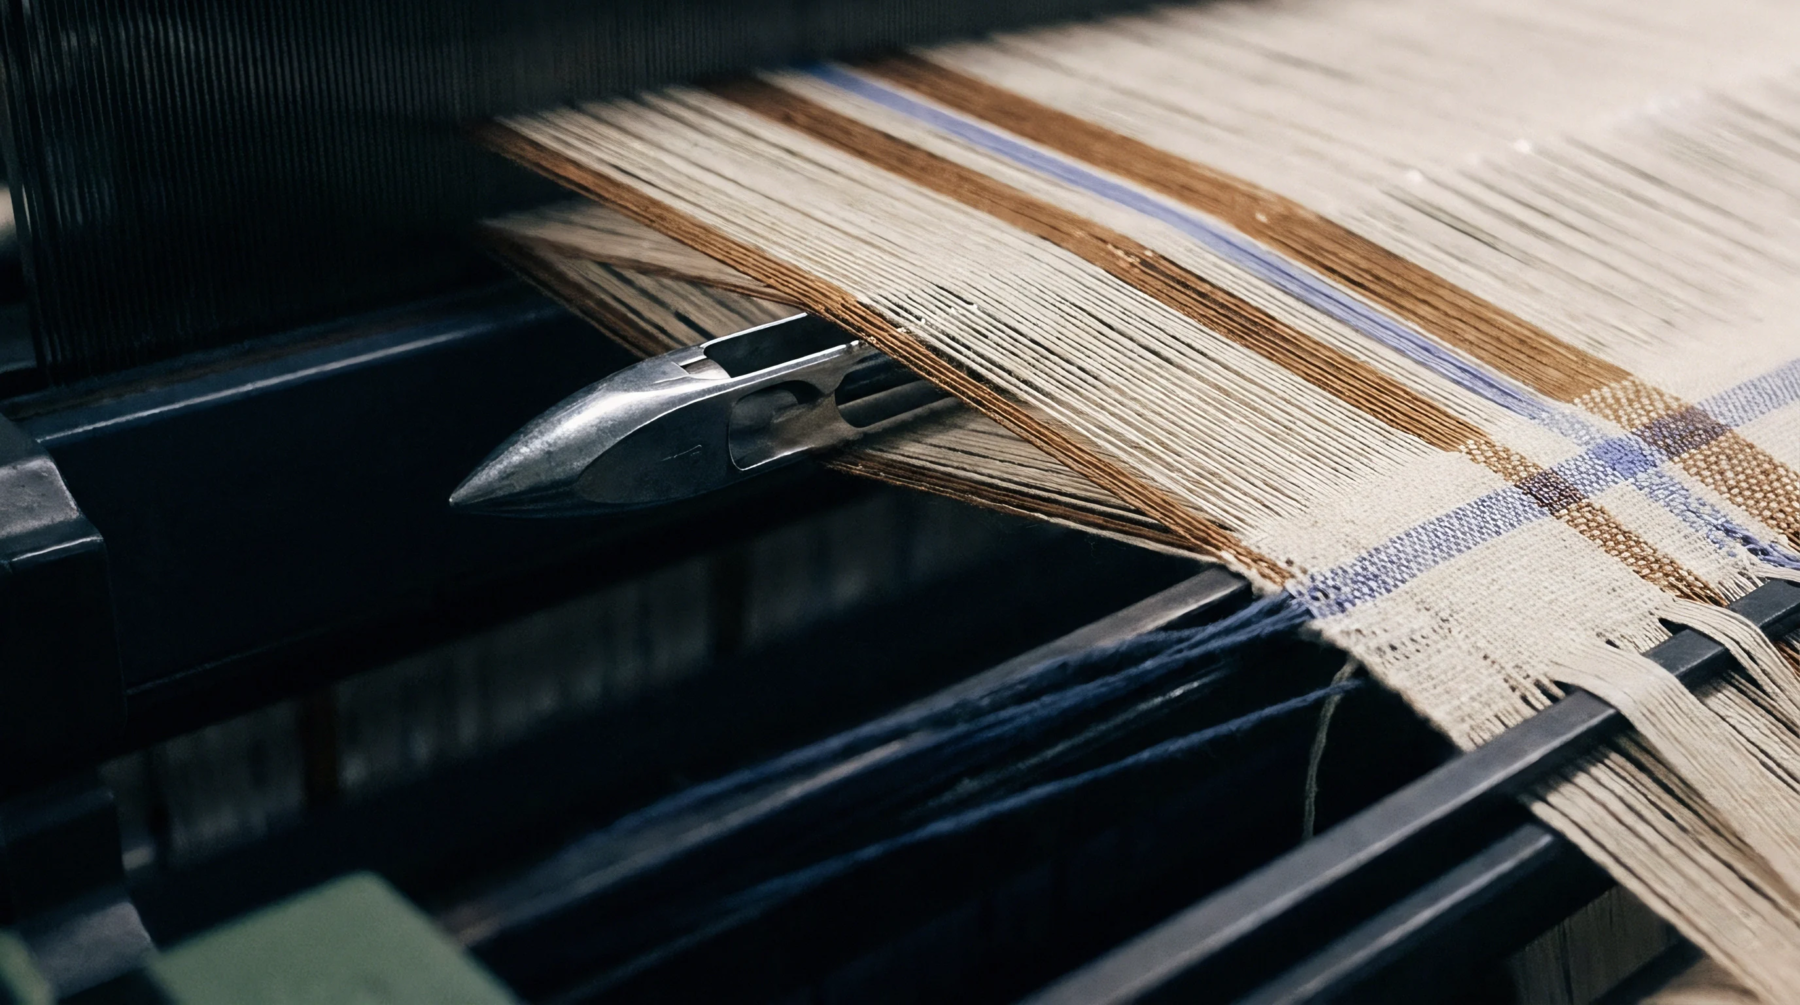
Reed Denting
Physical parameters governing the spatial distribution of warp ends inside a loom dictate the final width and linear mass of woven textiles. Thread density in reed quantifies the number of dents per unit measurement within the metal comb that separates individual warp yarns before they strike the fabric fell. Mills calculate this metric to establish correct sett specifications and prevent warp breakage during high-speed mechanical beating operations.
Production planners verify the count during loom setup to ensure finished greige goods meet contracted width specifications prior to wet processing.
Denting Geometry
Spatial arrangement inside the metal spacing combs dictates warp distribution and prevents adjacent ends from abrading during cyclic shed motion. Equipment operators insert specific quantities of warp yarns through each individual metal opening based on fabric structure requirements and yarn diameter constraints. Higher numerical counts require thinner metal blades to maintain adequate open area for shedding clearance and warp transport.
Excessive crowding inside restricted spaces generates frictional heat that strips size coatings from natural yarns and leads to operational stoppages.
Clearance Limits
Physical boundaries imposed by wire thickness and air space percentages restrict how many warp ends can pass through a single metal split without causing mechanical interference. Loom mechanics assess available air space alongside yarn diameter to determine maximum practical filling limits for specific loom types. Surpassing these structural limits forces adjacent warp lines into overlapping configurations that create visible reed marks and uneven surface texture in finished cloth.
Dense constructions require specialized denting patterns distributed across multiple rows to distribute mechanical stress evenly across the harness frames.
Spatial Verification
Quality inspectors measure the physical placement of warp yarns against production orders using optical magnifying glasses and graduated counting picks at the commercial inspection table. Discrepancies between targeted sett values and verified laboratory results indicate improper reed selection or incorrect drawing in procedures during loom preparation. Corrective actions involve replacing the metal comb with an alternative count before commercial shipment occurs.
Final acceptance depends on maintaining uniform spacing across the entire fabric width.