Managing Viscosity and Liquor Temperature Variance in Continuous Pad Batch Dyeing Systems
Jacketing troughs at twenty degrees Celsius and balancing roll nip deflection prevent reactive dye hydrolysis and side-to-center shade listing in pad batch runs.

Chill
Continuous pad batch systems operating with reactive dyestuffs depend on strict thermal suppression inside the application trough. When cellulosic piece goods enter the nip, reactive dyes encounter concentrated alkali additions designed to trigger fixation covalent bonding. Sodium hydroxide and sodium silicate introduce rapid exothermic heat spikes the moment dosing pumps inject them into water.
Uncontrolled bath warmth accelerates dye hydrolysis, destroying color value before cellulose absorption occurs. The production line loses head-to-tail shade depth within three hundred meters of continuous running.
Cold water lines feed the jacket.
Heat generation during alkali blending elevates trough temperatures by four to nine degrees Celsius above ambient plant water when external cooling loops remain inactive. Vinyl sulfone and heterobifunctional reactive chemistries exhibit extreme sensitivity to this thermal rise. At twenty degrees Celsius, reactive dye hydrolysis proceeds at a predictable, controlled rate that permits full diffusion into the fiber matrix.
Elevating that liquor to thirty degrees Celsius cuts the active dye half-life by more than half, forcing hydrolyzed dyestuff to sit uselessly in the liquor. The wash-off stages down the line face excessive unfixed color loads that compromise wet fastness ratings under ISO 105-C06.
A liquor temperature rise from twenty to thirty degrees Celsius reduces vinyl sulfone active bath stability from four hours to forty-five minutes under standard silicate alkali dosing.
Exothermic Dissolution and Pad Liquor Thermal Drift
Dosing units mix concentrated dye solution and alkaline fixatives immediately before liquor enters the trough, maintaining a standard four-to-one or five-to-one volumetric delivery. The pumps mix at four to one. Caustic soda hydration produces substantial enthalpy during dilution, warming the mixed feed before the fabric makes contact.
Without active heat exchangers on both incoming lines, the mixed liquor reaches twenty-eight degrees Celsius within ten minutes of continuous running. The greige fabric itself introduces residual thermal energy if drying cylinders after preparation ran hot without sufficient cooling skies.
Target values establish line speed.
The dyehouse manager observes gradual shade drift across large dye lots when trough temperature fluctuates between morning shifts and afternoon shifts. In winter production runs, incoming bore water sits at twelve degrees Celsius, suppressing dye dissolution and slowing core penetration. During summer months, unchilled facility water rises past thirty-two degrees Celsius, triggering premature hydrolysis inside the supply tubing.
Maintaining pad bath stability across twelve thousand meters demands constant chilling capacity linked directly to fluid monitoring sensors.
| Dye Reactive System | Trough Temperature (°C) | Fixation Half-Life (Minutes) | Hydrolysis Rate (% per Hour) | Total Shade Yield Loss (%) |
|---|---|---|---|---|
| Dichlorotriazine (DCT) | 18 | 45 | 4.2 | 2.1 |
| Dichlorotriazine (DCT) | 28 | 14 | 18.6 | 11.4 |
| Vinyl Sulfone (VS) | 20 | 120 | 2.8 | 1.5 |
| Vinyl Sulfone (VS) | 30 | 38 | 14.1 | 8.7 |
| Heterobifunctional (MCT/VS) | 22 | 180 | 1.9 | 0.8 |
| Heterobifunctional (MCT/VS) | 32 | 52 | 11.5 | 6.9 |
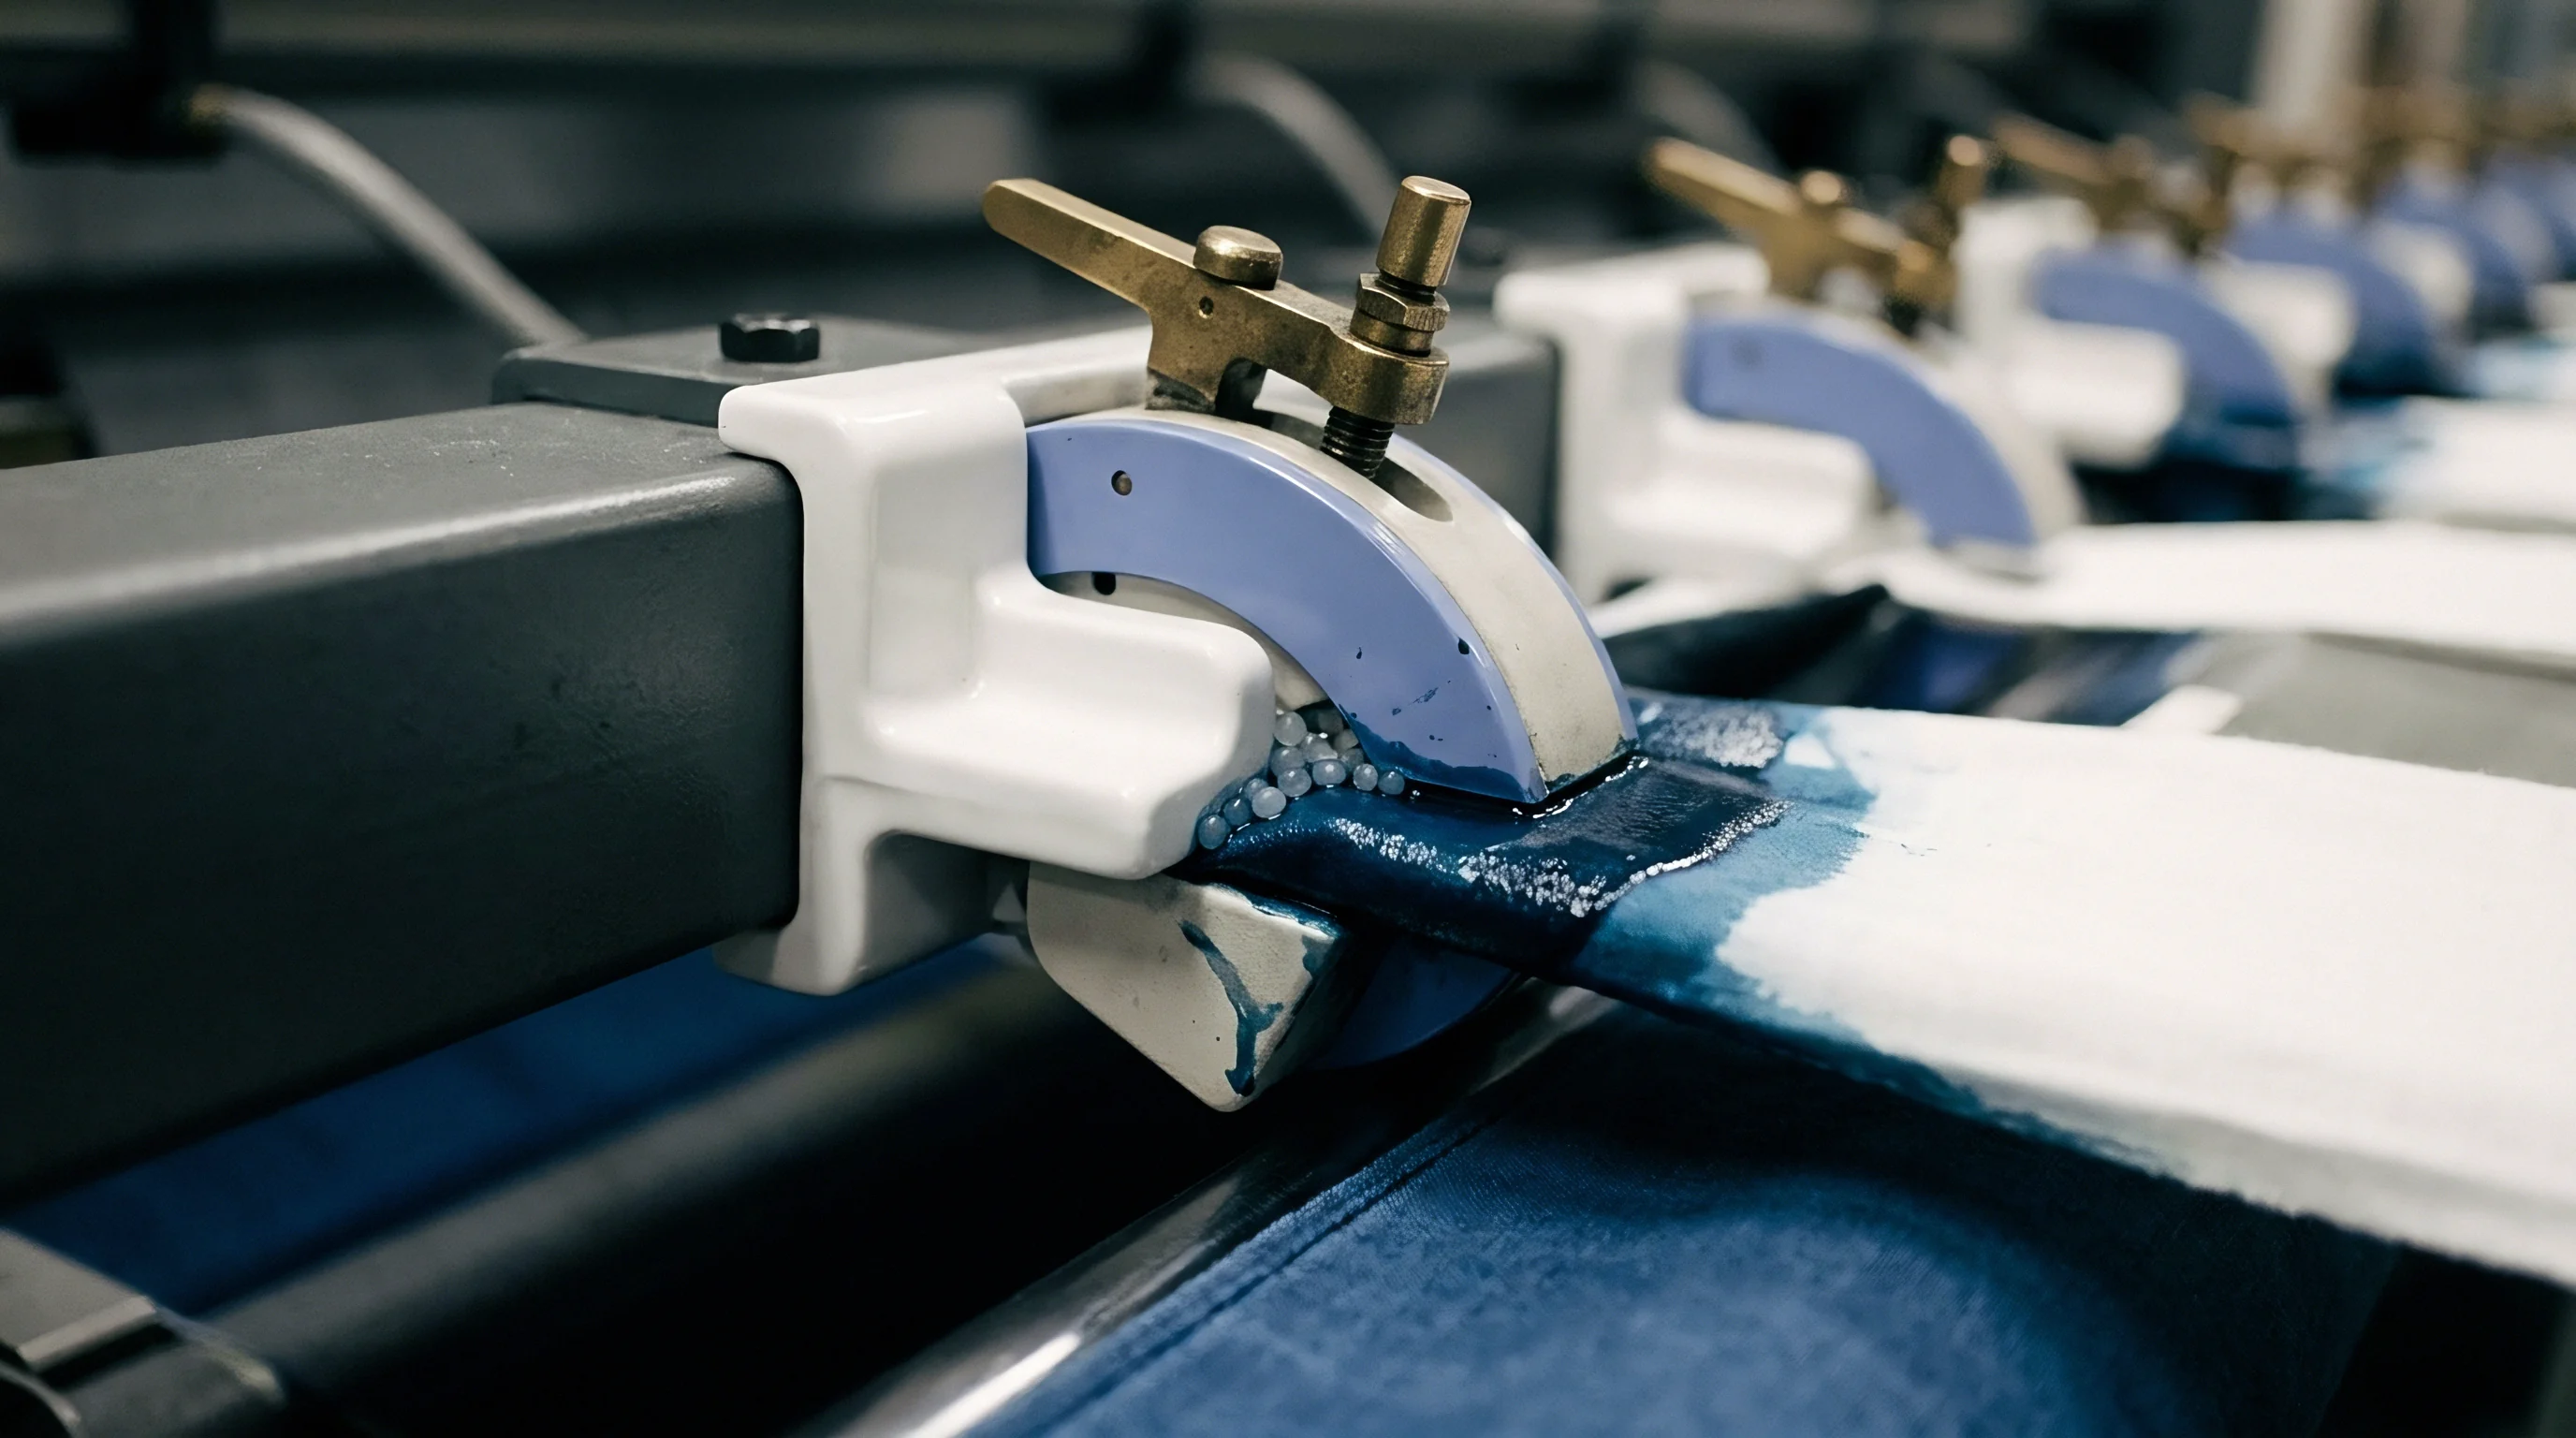
Low Volume Jacketed Troughs for Rapid Turnover
Minimizing fluid dwell time remains the primary physical defense against bath degradation. Modern continuous troughs utilize double-walled stainless steel construction circulating chilled glycol or cold brine at eight to twelve degrees Celsius. Trough residence drops below two minutes.
Reducing bath volume to ten or fifteen liters ensures incoming fresh dye and alkali replace the bath before chemical side-reactions escalate. Older thirty-liter troughs hold reactive liquor for seven to ten minutes at moderate fabric running speeds, permitting significant dye degradation at the liquid surface.
- Inline refrigeration chillers maintain closed-loop water circulation across the double jacket at ten degrees Celsius, absorbing thermal spikes from caustic soda dissolution.
- Electronic proportional valves modulate coolant volume according to immersion temperature sensors placed three millimeters below the fabric entry point.
- Secondary supply pre-coolers lower pure water stock tank temperatures to fifteen degrees Celsius prior to dyestuff dissolution cycles, preventing initial thermal elevation.
- Displacement wedge inserts eliminate dead circulation zones in trough corners, forcing rapid liquor consumption across wide loom widths.
Dyehouse managers routinely dismiss initial shade variations as natural batch-to-batch fiber variance, claiming the greige lot absorbed dye unevenly due to lingering natural cotton pectin.
Shear
Viscous properties inside the application bath govern how liquor transfers from the pad roll into the yarn bundle under pressure. Water-thin dye solutions behave differently than baths containing high sodium silicate concentrations or polymeric antimigrant thickeners. Sodium silicate adds considerable body to the formulation, raising dynamic resistance during high-speed saturation.
As production speeds climb toward seventy meters per minute, fluid shear rates inside the roller nip exceed several thousand reciprocal seconds, destabilizing non-Newtonian formulations. The cloth surface either rejects excess liquor or absorbs uneven chemical volumes across warp and weft intersections.
A wetting agent with inadequate low-foam characteristics causes micro-bubble entrainment under high nip shear that manifests as pale specks across high-sett poplin surfaces.
Viscosity governs liquid displacement.
Newtonian assumptions fail during high shear. Highly concentrated dyestuffs and electrolytes form transient polymer associations that thin under compression and thicken when stress ceases. When heavy plain-woven poplins or dense twills enter the nip, liquor viscosity determines whether the fluid moves into yarn interstices or simply pools on fabric surface valleys.
High viscosity limits bath penetration into tightly twisted ring-spun yarns, creating a ring-dyed cross section visible when cutting finished garments.

Does Viscosity Drift Dictate Pickup Uniformity?
Wetting dynamics determine the exact volume of chemical solution retained after the fabric clears the nip boundary. When viscosity drifts upward from thirty centipoise to eighty centipoise due to low temperature or heavy silicate dosing, the boundary layer of fluid dragged into the nip increases in thickness. The mechanical squeeze rolls push back against this viscous wedge, generating hydraulic lift that forces the rolls apart.
Wet pick-up increases unevenly, leaving the center of the fabric heavier in chemical saturation than the edges.
Cotton absorbs bath components selectively.
In offshore marine engineering, hydraulic control fluids maintain strict fluid shear stability to prevent valve failure in deep-sea actuators subjected to crushing pressures. Wet-processing padders face an identical fluid mechanic challenge: the chemical liquor must maintain stable viscosity across a extreme shear gradient inside the roller contact zone to prevent hydraulic separation of the steel cores. When pad formulations experience uncontrolled thinning, capillary wicking pulls water faster than dye molecules, establishing severe shade variation along the fabric length.
- Sodium silicate crystallization introduces micro-abrasives on the roller surface, tearing delicate filament warps and creating longitudinal dye streaks across continuous runs.
- Polymeric thickener agglomeration blocks the interstitial pores of dense canvas weaves, generating blotchy patches where dyestuff fails to penetrate inner yarn structures.
- Excessive surfactant concentration lowers bath surface tension below thirty dynes per centimeter, generating stable foam blankets that starve the nip center of chemical liquor.
- Temperature-induced thinning drops liquor viscosity below fifteen centipoise, causing gravity-driven bath drain lines down the fabric face before the batch roll can be wound.
Thickener Rheology under Nip Pressure
Sodium alginate and synthetic polyacrylate thickeners control liquor migration during the critical seconds between nip exit and batch winding. Alginate solutions exhibit pseudoplastic shear-thinning characteristics, flowing readily under mechanical nip stress and recovering immediate structural viscosity once the fabric exits the squeeze line. This recovery holds reactive dye molecules exactly where the nip pressed them, preventing gravitation toward the bottom selvedge of the rotating A-frame batch.
Synthetic acrylic thickeners often fail this rapid viscosity recovery, shearing cleanly under the roll but remaining too fluid for several seconds post-nip.
The thickest liquor always seeks the path of least mechanical resistance across the roller crown.
Squeeze
Mechanical pressure across the full roll face determines the final wet pick-up percentage of the saturated textile substrate. Standard industrial padders deploy deflection-compensated bowls to counteract the natural bending moments that occur when hydraulic cylinders apply tons of load to roll ends. Without internal compensation, the center of two opposing cylinders separates by fractions of a millimeter under load.
That microscopic deflection changes wet pick-up by five to twelve percent between fabric selvedges and the center, producing uncorrectable side-to-center shade bands.
Rollers flex under pneumatic loading.
Pick-up drifts across wide beams.
Rubber covering hardness directly dictates nip contact area and pressure distribution profiles. Covering compounds rated at seventy to seventy-five Shore A hardness deliver an optimal twelve-to-fifteen-millimeter contact stripe under standard four-bar line pressure. Softer rubber coverings below sixty-five Shore A broaden the contact zone, lowering peak hydraulic pressure and leaving excess surface liquor on textured weaves.
Harder coverings above eighty Shore A compress minimally, creating extreme pressure peaks that crush delicate twill ribs and cause mechanical yarn glazing.
Gravimetric strip testing according to ISO 3801 demonstrates that a three percent differential in wet pick-up across the fabric width generates a visible Delta E shift exceeding 0.8 under D65 illumination.
Deflection Compensation across the Bowl Width
Swimming rolls and internally supported piston-loaded bowls counteract roll bending through internal hydraulic chambers. Floating roller designs feature a stationary central axle surrounded by a rotating outer steel cylinder supported on hydraulic oil pads. Technicians adjust the hydraulic pressure inside the stationary core to match the external loading cylinders precisely.
If external air pistons press at three point five bar, internal hydraulic oil chambers require corresponding pressure to maintain a parallel gap across two meters of roller face.
Routine maintenance teams measure roll profiles using carbon paper impression impressions or electronic pressure-sensing film pulled through the nip at creeping speed. The contact stripe must measure identical width at the left selvedge, center point, and right selvedge within a tolerance of zero point five millimeters. Hardness discrepancies develop when rubber coverings age unevenly or absorb chemical plasticizers from aggressive solvent scours left in prepared greige goods.
Grinding schedules every nine to twelve months restore the true cylindrical profile and remove oxidized surface skins.
| Roll Position | Rubber Hardness (Shore A) | Nip Stripe Width (mm) | Measured Pick-Up (%) | Delta E (CIELAB D65) | Tensile Loss (Warp N) |
|---|---|---|---|---|---|
| Left Selvedge | 72 | 14.2 | 66.2 | 0.22 | 840 |
| Left Center | 71 | 14.8 | 68.5 | 0.54 | 835 |
| Center | 70 | 15.5 | 71.8 | 1.18 | 820 |
| Right Center | 71 | 14.7 | 68.1 | 0.48 | 838 |
| Right Selvedge | 73 | 14.0 | 65.8 | 0.18 | 845 |
| Data gathered on 210 g/m² 3/1 cotton twill under 4 bar pneumatic loading, target pick-up 65.0%, evaluated under ISO 105-J03 color difference criteria. | |||||
Expression Modeling and Color Yield Variations
Calculating the relationship between expression percentage and actual dye molecule deposit reveals direct links to shade depth. Take an application recipe containing forty grams per liter of reactive black mix on a 210 g/m² cotton drill. At sixty-five percent target pick-up, one kilogram of dry cotton retains six hundred and fifty grams of bath, delivering twenty-six grams of active dye powder into the fiber structure.
If deflection issues raise the center pick-up to seventy-two percent, the center retains seven hundred and twenty grams of bath, carrying twenty-eight point eight grams of dye.
The resulting two point eight gram dye excess per kilogram of fabric shifts color depth far beyond acceptable visual boundaries. Spectrophotometric scans read this variance as a prominent dark stripe down the fabric center. The dyehouse cannot scour out the defect because reactive dyes fix permanently in proportion to active molecules present during the alkaline dwell stage.
The finisher cannot correct this fault in post-treatment stenter frames without stripping the entire lot with aggressive reducing agents that degrade cellulose fiber chains.
Failure to calibrate squeeze pressures across the bowl face forces entire dyed batches into secondary dye lots or salvage markets at forty percent below contracted invoice value.
Dwell
Batching operations hold wet, alkaline-impregnated piece goods on rotating A-frames while covalent dye-fiber bonding concludes. The fabric roll must remain perfectly cylindrical and smoothly wound to prevent localized pressure bands. The batch rotates continuously.
Mechanical drives turn the roll at six to eight revolutions per minute throughout the dwell cycle, which spans four to twenty-four hours depending on dye reactiveness and alkali chemistry. Halting rotation allows gravitational force to drain liquid downward, creating a two-tone shade difference between the top and bottom edges of every wrapped layer.
Peripheral edges dry out first.
Environmental conditions surrounding the batching area exert direct influence over fixation percentages. Ambient hall temperatures below eighteen degrees Celsius stall the chemical reaction between dye vinyl sulfone groups and cellulose hydroxyl ions, leaving dyestuff unattached. Conversely, batching in hot summer zones exceeding thirty-five degrees Celsius triggers moisture evaporation from exposed outer layers and selvedges.
Water loss concentrates the alkaline salts locally, causing severe edge burning, fabric tendering, and profound shade darkening on outer roll wraps.
Wrapping the entire batch roll in heavy polyethylene film immediately upon nip exit blocks surface moisture loss and shields the fabric from atmospheric carbon dioxide neutralization.
Will Ambient Floor Swings Undermine Fixation?
Seasonal factory temperature shifts alter fixation kinetics significantly across extended dwell intervals. When reactive vinyl sulfone dyes dwell with sodium silicate at twenty-two degrees Celsius, complete fixation requires twenty to twenty-four hours of stable rotation. If nighttime plant temperatures plummet to twelve degrees Celsius, chemical reaction rates drop by more than sixty percent.
The lot arrives at the washing range with unreacted dyestuff that strips away down the drain, resulting in pale, out-of-spec shades.
Atmospheric carbon dioxide acts as a mild acid gas that neutralizes exposed surface alkalis over long holding times. Unwrapped roll faces absorb ambient carbon dioxide, converting active sodium hydroxide into sodium carbonate. The resulting drop in surface pH halts reactive dye fixation along outer winds, leaving the exterior twenty meters of fabric noticeably lighter than the roll core.
Protective wrapping maintains the internal microclimate and seals the surface against acid-gas contamination.
Hydrolysis Boundaries and Rotation Speed
Rotational stability governs liquid distribution throughout the porous textile matrix during batch storage. High winding tension stretches wet cellulose fibers, closing yarn pores and squeezing chemical liquor toward the roll edges. Low winding tension creates loose, soft rolls that sag into an eccentric oval on the A-frame beam, producing erratic pressure points as the uneven roll turns.
Calibrated center-wind tension controls maintain constant packing density from the cardboard core to the final exterior wrap.
- Tension transducers adjust winding torque progressively as roll diameter expands, preventing core crushing and longitudinal telescoping.
- Polyethylene stretch-wrap stations apply three overlapping plastic barriers across the rotating beam, sealing selvedges against atmospheric carbon dioxide ingress.
- Climate-controlled batching bays house rotating A-frames inside enclosed corridors regulated at twenty-two degrees Celsius, dampening floor temperature swings.
- Continuous rotation monitoring switches trigger auditory plant alarms if mechanical motor drives stall for longer than ninety seconds during storage cycles.
The degree to which microscopic moisture migration continues between tightly wound inner cotton layers throughout eighteen hours of continuous turning remains an open technical controversy.
Margin
Commercial contracts for dyed piece goods hinge on strict instrumental color tolerances and finished structural performance specifications. When pad-batch liquor temperature and viscosity wander unchecked, the resulting yardage fails CIELAB Delta E thresholds under standard retail illuminants. Buyers reject lots showing side-to-center shading above zero point eight Delta E CMC (2:1), knowing cutting rooms cannot lay out patterns across variable shade profiles without producing two-tone garment panels.
The converter faces substantial financial penalties when goods fail four-point fabric inspection protocols under ASTM D5430.
Uncut yardage sits on hold.
The buyer withholds final balance.
Tight tolerances protect seam margins.
Fabric construction specifications establish performance baselines that continuous pad batch processing must preserve. A 2/1 twill woven with thirty combed cotton warps and twenty-four ring-spun wefts must maintain minimum ISO 13934-1 tensile strength targets of seven hundred Newtons in the warp. When excessive pad liquor temperatures force multiple stripping and re-dyeing cycles, boiling alkaline baths and hydrosulfite strips dissolve cellulose chain polymers.
The fabric loses fifteen to twenty-five percent of its burst and tear resistance, turning commercial grade cloth into unusable scrap that fails minimum apparel garment requirements.
Tolerances for Side to Center Variance
Finished goods specifications enforce strict spectrophotometric checks across five distinct points per roll: left selvedge, left center, center, right center, and right selvedge. Testing follows ISO 105-J03 color difference standards, evaluating differences against the approved customer submission swatch under D65, TL84, and Illuminant A lighting. Side-to-center shading exceeding zero point six Delta E creates visible color mismatches when adjacent garment panels meet at seams.
In plain woven shirting, even zero point five Delta E variance between sleeve and body sections triggers retail garment rejections.
The route from greige mill to finished export shipping carton leaves zero commercial space for wet processing error. If a lot exhibits center listing due to crowned roller deflection or high fluid viscosity, the converter cannot blend the issue away in tentering or compacting. The defect runs the full length of the run, ruining thousands of meters of continuous fabric.
Shifting production to secondary markets reduces the value per finished meter by half, eradicating the converter margin and transferring severe recovery costs onto the commission dyehouse.
Contract Mechanics for Dyehouse Lot Rejections
Purchase orders must delineate exact procedural boundaries for batch acceptance and financial liabilities. Clear contract agreements state the specific test standards, sampling intervals, and instrumental equations used to evaluate shade uniformity. When dispute procedures arise over rejected continuous yardage, commercial arbiter panels examine mill inspection dossiers for logged padder temperature sheets and roller maintenance charts.
Contracts that incorporate standard commercial arbitration lines dictate that any dye lot exhibiting cross-width color variance above 0.8 CMC 2:1 under Illuminant D65 permits the buyer to cancel subsequent supply orders immediately, forfeit the conversion fee, and assess full greige replenishment costs directly against the finishing facility.