Resolving Multi-Axial Specular Surface Refraction in High Speed Heterogeneous Microfiber Web Inspection
Cross-polarized darkfield line-scan arrays eliminate specular glint on bicomponent microfibers, cutting false defect scrap rates below one percent.
Glint
High-speed line-scan cameras running over synthetic nonwoven webs at eight hundred metres per minute register hundreds of false alarms every second when unpolarized lighting hits cleaved microfibers. Individual filament diameters in splittable bicomponent webs range from 0.1 to 0.4 dtex. When mechanical hydroentanglement splits an 80/20 polyester and polyamide composite filament into sixteen or thirty-two distinct wedge segments, each exposed polymer facet creates an independent cylindrical mirror.
The sensor saturates instantly. Line cameras reading three-micrometre pixel footprints capture sudden brightness spikes that look identical to melt spots, pinholes, or calendar burns. The physical web contains no structural failure at that coordinate.
The signal spike originates purely in directional specular refraction bouncing off angled filament boundaries directly into the collection aperture.
A thirty-degree shift in illumination azimuth reduces false positive glare spikes by fourteen decibels across hydroentangled polyester surfaces.
Surface scattering across nonwoven webs depends directly on filament cross-sectional geometry, web density, and line velocity. When examining technical wiping substrates, synthetic suede bases, or precision filtration media, inspection systems encounter multiple distinct optical distortions:
- Specular flare bursts overload linear sensor arrays whenever filament facets align perpendicular to the incident ray path.
- Refractive internal reflections channel light through high-index polyester segments before discharging concentrated beams toward the camera lens.
- Diffraction halo patterns generate false edge-defect triggers across tightly spaced micro-filament bundles.
- Shadow cavitation artifacts simulate severe thin-spots behind raised surface loops in spunlace structures.
False rejections multiply rapidly. Converting mills set defect classification algorithms to catch three-hundred-micrometre foreign particles or broken filaments. When specular reflections generate intensity deltas exceeding seventy gray levels on an eight-bit scale, automated rejection gates divert prime yardage into waste bins.
Inspecting these heterogeneous surfaces demands decoupling directional specular glare from true structural web flaws. Uncorrected specular saturation causes whole production lots to face unjustified downgrade to secondary wiping grades at a thirty percent discount.
Matrix
Extrusion lines spinning pie-wedge or island-in-the-sea filaments combine polymers with fundamentally incompatible optical indices. Polyethylene terephthalate exhibits an isotropic refractive index near 1.58, accompanied by drawing-induced birefringence that elevates the longitudinal refractive index to 1.71 while the transverse index drops to 1.54. Polyamide 6 maintains an isotropic index near 1.53, with drawn values reaching 1.58 along the fibre axis.
Refractive index mismatches generate flare. When high-pressure water needles split the bicomponent segments during hydroentanglement, exposed triangular surfaces face outward at arbitrary orientations across three dimensions. Incident rays striking a polyamide-polyester interface refract across severe optical gradients, turning each split fiber bundle into an irregular prism cluster.
Polymer Birefringence across Cleaved Wedge Geometries
Filament cross sections dictate scattering. A segmented pie configuration presents sharp wedge corners that focus transmitted light along acute axes. Island-in-the-sea filaments present thirty-seven or sixty-four sub-denier circular fibrils suspended inside a sacrificial matrix.
Once chemical extraction dissolves the matrix polymer, the remaining micro-fibrils collapse into dense mats with high surface roughness. The optical behavior changes completely between these two cross-sectional architectures, shifting from directional planar reflection to diffuse volume scattering.
| Polymer Composition | Cross-Sectional Shape | Longitudinal Index | Transverse Index | Birefringence Delta | Reflectance Percentage |
|---|---|---|---|---|---|
| Polyethylene Terephthalate | Sixteen-Segment Wedge | 1.712 | 1.544 | 0.168 | 5.85 |
| Polyamide 6 | Sixteen-Segment Wedge | 1.580 | 1.528 | 0.052 | 4.41 |
| Polypropylene | Trilobal Homofilament | 1.530 | 1.496 | 0.034 | 4.32 |
| Polybutylene Terephthalate | Islands-In-Sea Fibril | 1.640 | 1.535 | 0.105 | 5.12 |
| Polylactic Acid | Round Homofilament | 1.462 | 1.455 | 0.007 | 3.45 |
Bicomponent filament splitting is rarely uniform across commercial nonwoven rolls. Quantitative chemical analysis under standard ISO 1833 reveals nominal 80/20 polyester-polyamide formulations that fluctuate by plus or minus 2.5 percent across transverse web positions. Incomplete mechanical cleavage leaves un-split precursor fibres measuring 2.2 dtex directly adjacent to fully cleaved 0.15 dtex micro-filaments.
The un-split filaments preserve their cylindrical geometry, reflecting light as intense longitudinal lines rather than broad diffuse clouds. Machine vision cameras interpret these intense linear reflections as foreign mono-filament contamination or warp-wire pickup from forming belts.
Filament splitting yield below ninety percent quadruples surface glint variations by preserving cylindrical precursor geometries.
Differential polymer cooling during spin-pack extrusion introduces residual molecular stresses that shift regional refractive indices. When drawn at draw ratios between 3.2 and 3.8, crystalline orientation develops along preferred directions, creating non-uniform extinction angles under cross-polarized light. Extrusion houses routinely claim that pie-wedge segment variation reflects normal thermal die swell rather than poor melt viscosity control.
Beam
Line illumination geometry governs whether an automated inspection sensor sees physical defects or optical noise. Conventional diffuse brightfield lighting fails completely on cleaved microfibers because omnidirectional light illuminates every possible facet angle simultaneously, burying low-contrast defects inside a background of continuous specular glint. Resolving web anomalies at line speeds exceeding ten metres per second requires structured, multi-axial lighting rigs combined with polarizing filters aligned to extinguish primary surface reflections.
Where Does Polarized Illumination Suppress Specular Glare?
Line generators equipped with linear polarizing sheets project light with an electric field vector oriented parallel to the cross-machine direction. Camera lenses fitted with high-extinction linear analyzers oriented in the machine direction block this polarized specular reflection completely. Extinction ratios decide signal clarity.
Standard sheet polarizers provide an extinction ratio of 10,000:1 at 632 nanometres, eliminating ninety-nine percent of direct facet reflections while allowing depolarized diffuse light scattered from deeper web structures to pass into the camera sensor.
Birefringent fibers complicate this clean polarization extinction. High-tenacity polyester rotates the polarization plane of light penetrating the fiber sheath, re-emitting refracted rays with elliptical polarization states that pass directly through cross-polarized analyzers. Line rates exceed ten meters per second.
The cross-polarization setup eliminates direct surface glare from polyamide segments while highlighting subsurface strain variations inside polyester cores. Inspection engineers separate these competing signals by deploying dual line-scan bars, where the first sensor captures cross-polarized reflectance while the second captures unpolarized darkfield scatter.
Darkfield Spatial Separation in Line Sensors
Positioning light bars at low grazing angles between ten and twenty-five degrees relative to the web surface transforms inspection sensitivity. Grazing incidence prevents specular reflections from entering normal-incidence camera lenses. Only structural web anomalies, including raised clumps, un-split filaments, foreign fly waste, and calendar puncture holes, scatter grazing light upward into the collection optics.
| Inspection Channel | Illumination Angle | Polarizer Orientation | Target Defect Mechanism | Signal Ratio Threshold |
|---|---|---|---|---|
| On-Axis Brightfield | 85 to 90 Degrees | Co-Polarized Linear | Web density shifts, holes | 12 dB |
| Cross-Polarized Field | 75 to 80 Degrees | Crossed 90 Degrees | Melt drops, resin spots | 22 dB |
| Forward Darkfield | 15 to 25 Degrees | Unpolarized High-Power | Loose fibers, loop pile | 18 dB |
| Backlight Transmission | 180 Degrees Inline | Unpolarized Diffuse | Pinholes, void mapping | 28 dB |
Aligning multi-channel optical systems on moving production equipment demands strict physical calibration sequences:
- Mechanical web stabilization must eliminate vertical sheet fluttering within fifty micrometres across vacuum inspection rolls.
- Illumination focal positioning concentrates light energy into a two-millimetre band across the full web width.
- Polarizer angle fine-tuning rotates the receiving analyzer until sensor baseline counts drop below twenty gray levels under bare web conditions.
- Pixel response normalization balances photo-response non-uniformity across all sixteen thousand elements on the line-scan sensor array.
Line scan encoders track motion. Web tension variations cause fluttering over open spans, moving the microfiber surface outside the optical depth of field, which rarely exceeds 1.2 millimetres at high optical magnification. Vacuum transfer tables stabilize the substrate, ensuring that illumination angles remain locked relative to the camera axis across five-hundred-metre roll packages.
Optical engineers continue to debate whether circular polarization arrays can suppress multi-axial filament refraction across high line speeds without sacrificing light throughput on dark spunlace substrates.
Finish
Spin-finish oils applied to filament bundles prior to hydroentanglement alter the refractive boundary of the entire web. Synthetic fiber producers apply mineral oil, ethoxylated fatty acids, or polyorganosiloxanes at concentrations between 0.4 and 1.2 percent by weight to control static electricity and promote smooth drafting through carding machines. Residual spin-finish creates thin liquid films spanning adjacent microfibers.
Oil droplets act as micro lenses. These tiny liquid menisci possess a refractive index near 1.48, bridging the air-polymer gap and forming smooth refractive surfaces that intensify specular reflections by concentrating scattered light into tight focal beams.
Topical Lubricant Pools on Moving Webs
Spunlace washing stages remove topical lubricants unevenly across wide production lines. Web sections retaining higher oil concentrations display higher optical gloss, skewing automated grey-level baselines by thirty percent. Spinning oils migrate under line tension.
When calendar rolls heat the damp web, residual lubricants collect in localized surface pools, creating optical glints that automated inspection cameras flag as synthetic resin contamination.
A finish concentration delta of zero point three percent across roll widths shifts optical reflectivity thresholds by twenty-five gray levels.
Classing technicians verifying raw bale stock assess spin finish levels using Soxhlet extraction with petroleum ether under test standard ISO 10580. A laboratory result showing 0.8 percent total extractable matter on raw staple fiber indicates high risks for specular lensing unless the downstream hydroentanglement line operates high-pressure de-watering vacuums and extensive wash boxes. Clean water jets displace surfactant layers, breaking up the microscopic meniscus lenses that generate false glare spikes under line-scan cameras.
Excess finish always mimics un-cleaved wedge faults under grazing illumination.
Threshold
Discriminator logic operating in high-speed inspection software separates physical defects from optical artifacts by analyzing spatial frequency and aspect ratios. True nonwoven defects exhibit measurable dimensional persistence across consecutive scan lines. A broken filament extends longitudinally across dozens of lines; an oil drop or foreign particulate forms a multi-pixel two-dimensional cluster; a mechanical puncture breaks web continuity across both machine and cross-machine directions.
In contrast, specular glints originating from microfiber facets persist across only one or two scan lines because web flutter and shifting viewing angles rapidly break the specular reflection condition.
Spatial Filtering and Phantom Defect Discrimination
High-pass spatial filtering isolates sharp pixel transitions while low-pass filters map broad basis-weight shifts. When a 16K line-scan camera samples a web at forty kilohertz, specular glints appear as high-frequency impulse noise. Convolution kernels sized at three by three pixels eliminate single-pixel intensity spikes without diminishing the optical signature of true half-millimetre contamination specks.
Unsplit segments mimic resin globs.
| Target Feature | Pixel Dimension | Intensity Delta | Persistence Across Lines | True Defect Status |
|---|---|---|---|---|
| Specular Facet Flare | 1 x 2 Pixels | +80 Gray Levels | 1 to 2 Lines | False Positive Artifact |
| Residual Oil Meniscus | 2 x 3 Pixels | +45 Gray Levels | 2 to 4 Lines | False Positive Artifact |
| Un-Split Wedge Bundle | 2 x 40 Pixels | +65 Gray Levels | 30 to 80 Lines | Process Defect Flaw |
| Polymer Melt Clump | 8 x 8 Pixels | -90 Gray Levels | 15 to 25 Lines | Critical Structural Defect |
| Forming Wire Hole | 12 x 10 Pixels | +120 Transmission | 20 to 30 Lines | Critical Void Failure |
| Cotton Fly Trash | 6 x 14 Pixels | -70 Gray Levels | 10 to 20 Lines | Foreign Contamination |
Line integration settings control signal-to-noise margins. Time Delay Integration line sensors accumulate charges across multiple sensor stages, boosting light capture without demanding destructive illumination wattages that melt heat-sensitive microfibers. Charge accumulation averages out single-line glints across sixty-four or one-hundred-twenty-eight stages, providing smooth background imagery where structural defects stand out clearly against the diffuse fiber mat.
Auditing finished roll goods requires evaluating clear quality acceptance thresholds:
- Optical noise margin verification sets baseline camera gain so maximum fiber scatter never exceeds thirty percent of digital saturation.
- Aspect ratio filtering rules reject all single-axis bright spots exhibiting length-to-width ratios below 1.5 when area spans less than four pixels.
- Multi-camera coincidence gating registers an alarm only when both cross-polarized reflectance and low-angle darkfield channels report simultaneous coordinate matches.
- Defect clustering density limits flag rolls for physical inspection whenever localized false-alarm clusters exceed five events per square metre.
Off-spec lots face immediate rejection. Sourcing engineers drafting purchasing agreements define inspection rules based on verified defect density rather than raw camera alarm counts. Incorporating standard inspection clause ASTM D5430 Four-Point scoring into the supply contract forces automated scanners to disregard single-pixel transients below one millimeter in length.
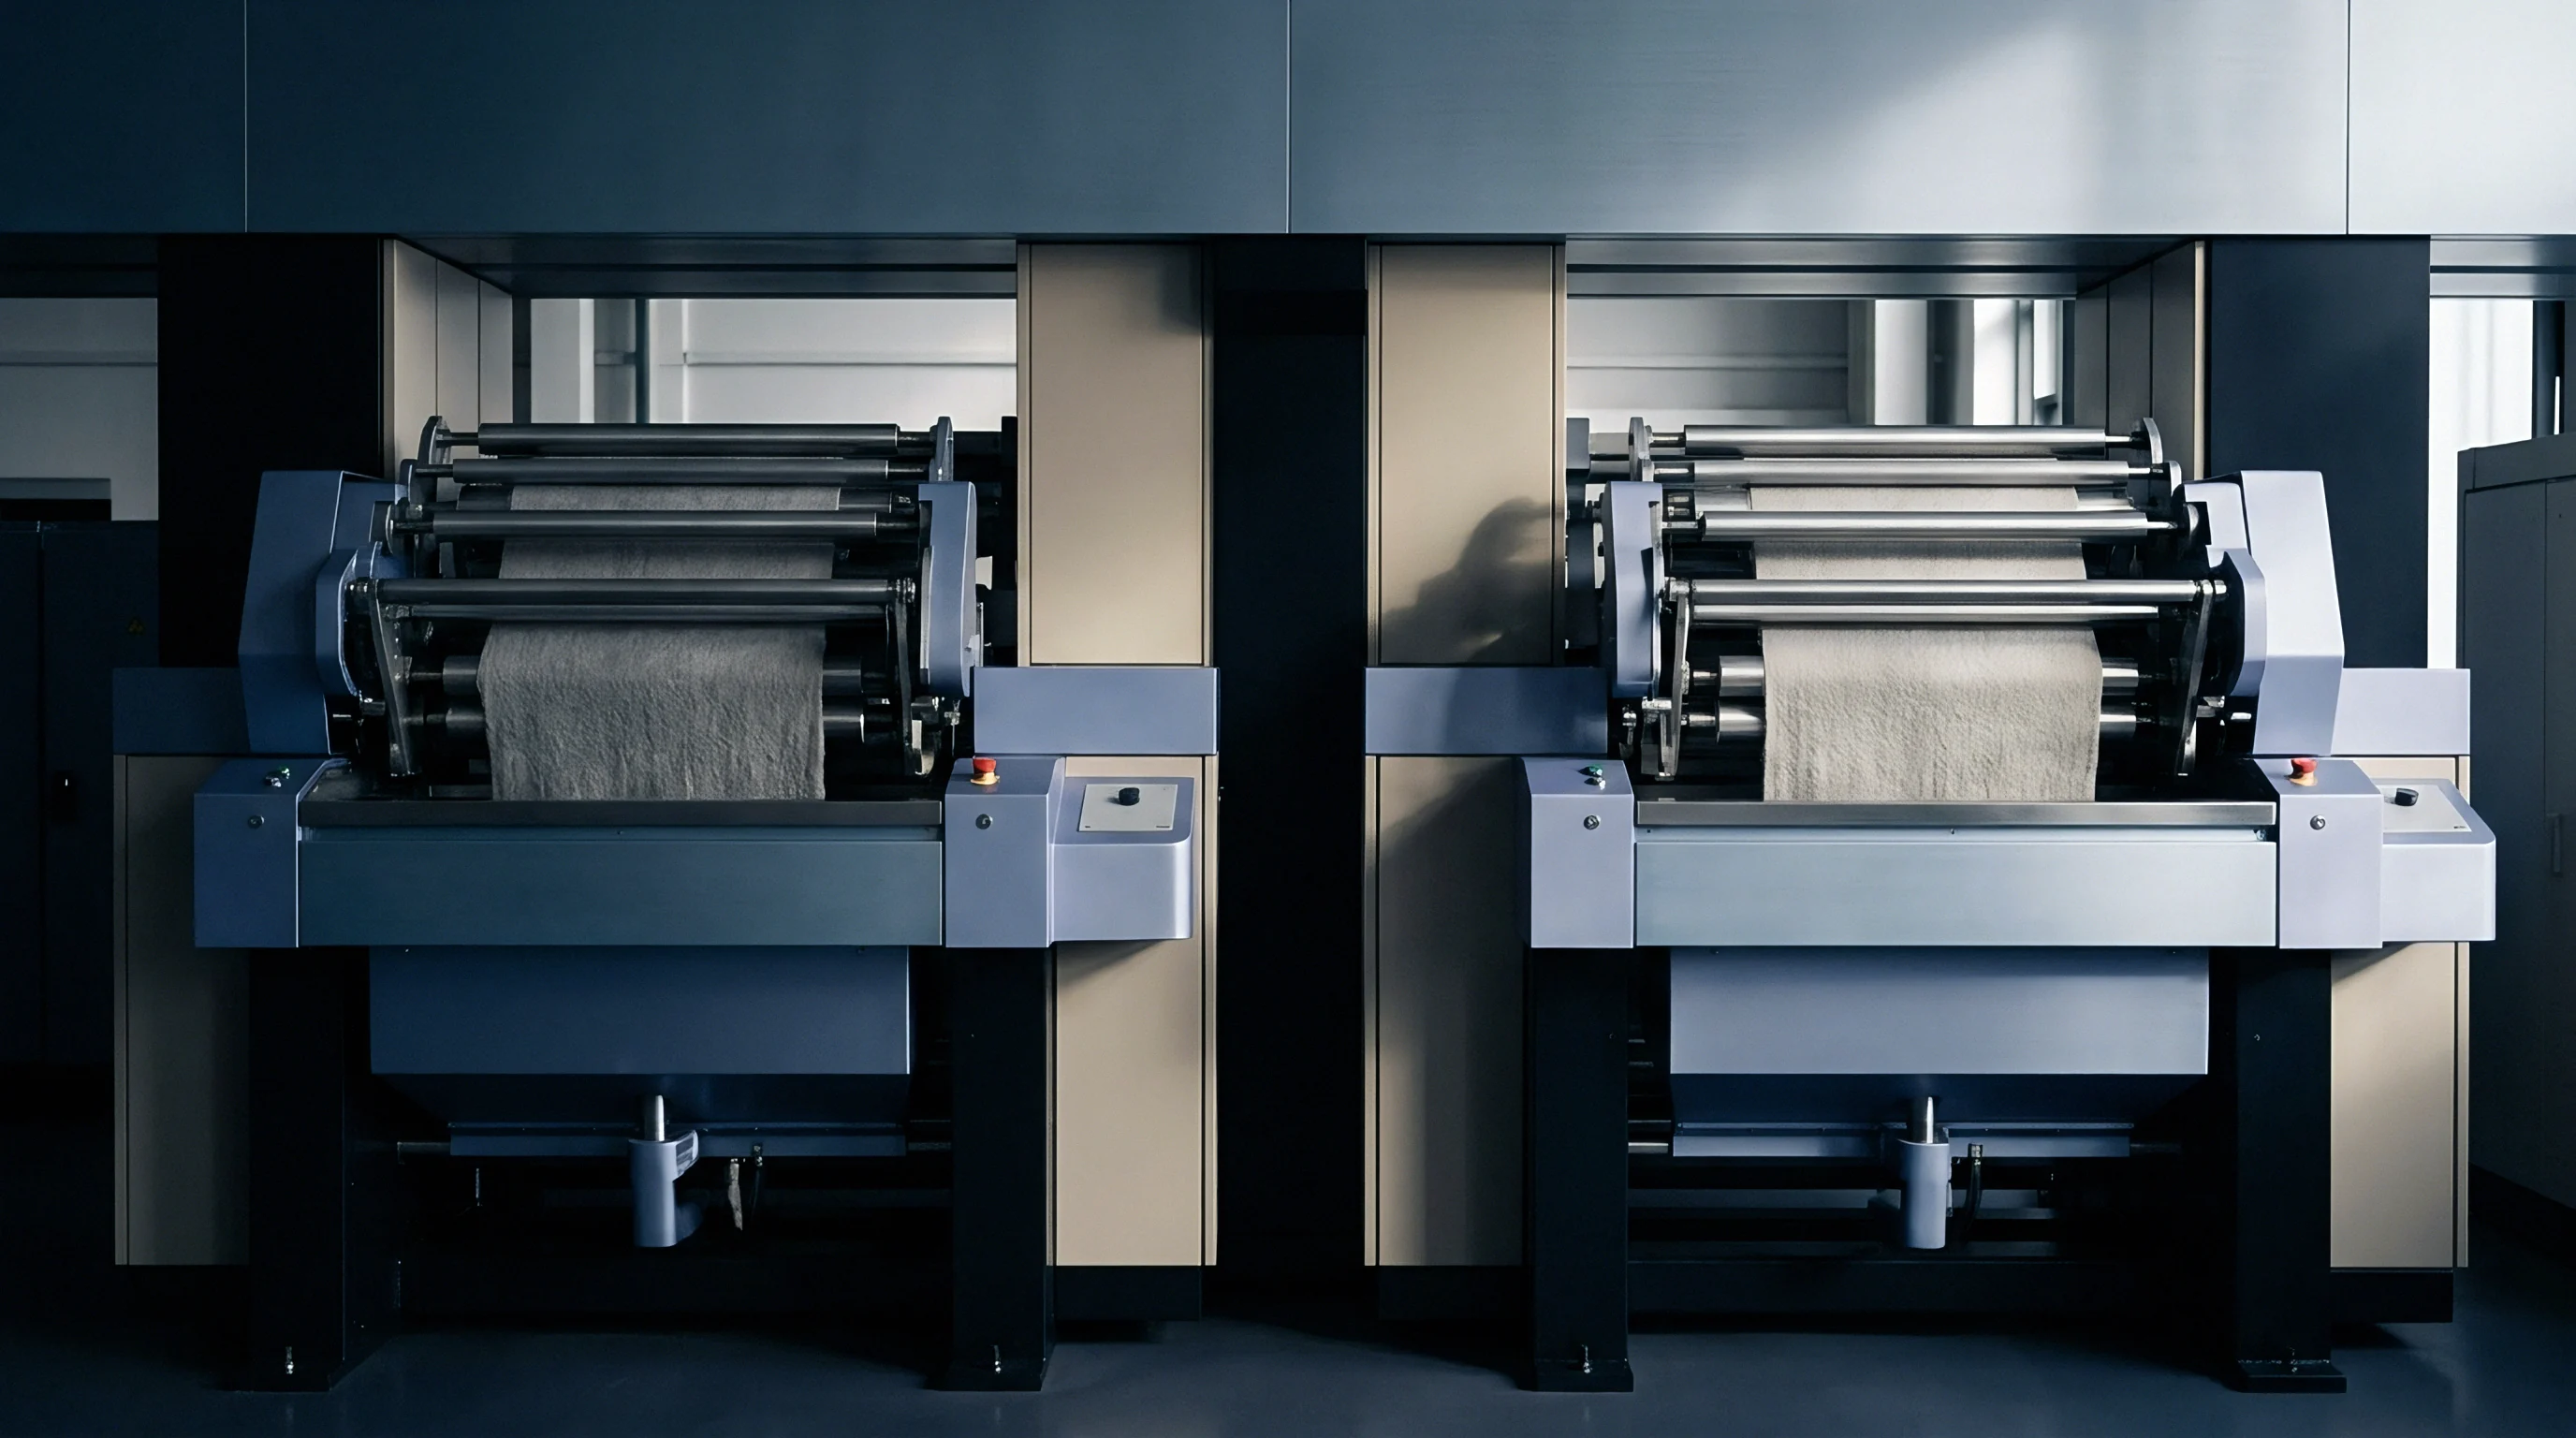
Invoice
Customs declarations and final settlements depend heavily on verifiable web quality grades. Clean hydroentangled microfibers classified under Harmonized Tariff Schedule heading 5603 for nonwovens clear borders at distinct duty rates depending on weight per square metre. Goods weighing between twenty-five and seventy grams per square metre carry specific customs valuations that reflect high-end industrial wiping, filtration, or apparel lining applications.
If optical inspection systems register rampant false defect counts, mills down-grade the material to utility wipes, slashing invoice values from 4.80 dollars per kilogram to 2.10 dollars per kilogram.
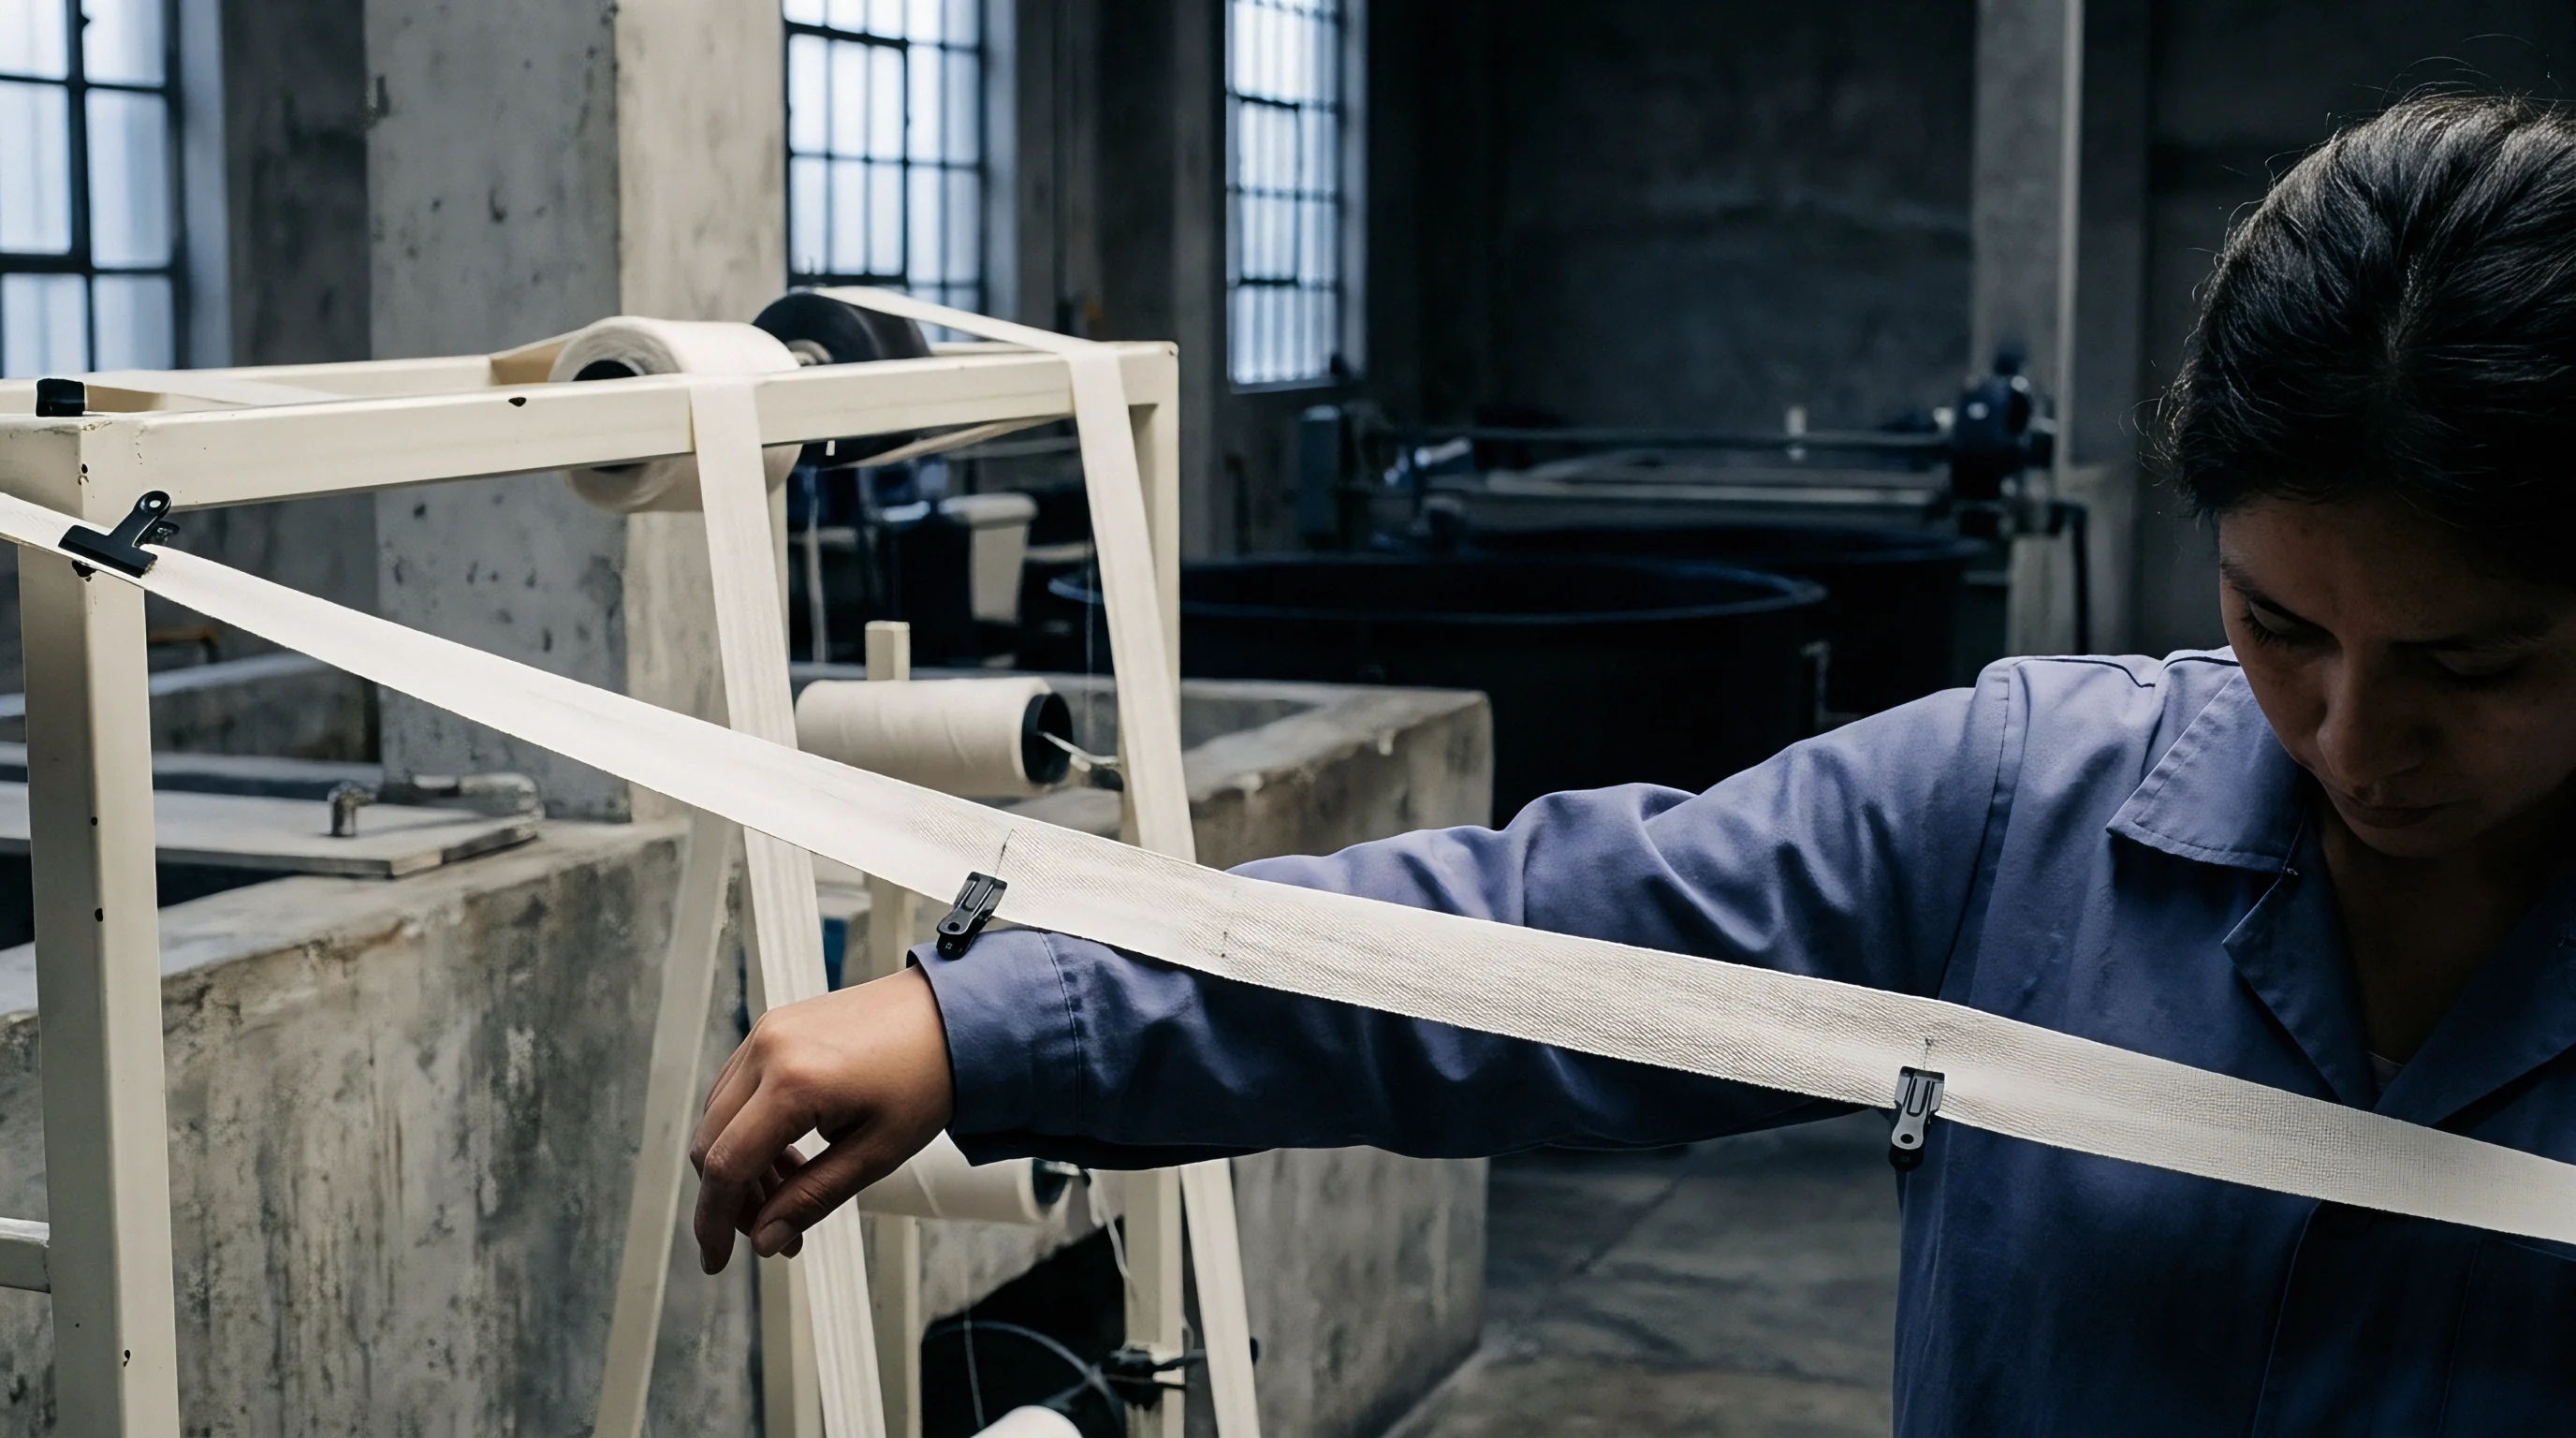
Settlement Deductions on Optical Reject Grades
When an automated optical inspection gate halts an automated slitter rewinder due to specular glare spikes, production costs spiral immediately. Slitter downtime costs converting facilities upwards of eight hundred dollars per hour in lost throughput. If optical logs generate dispute files claiming thirty defect points per one hundred square metres on rolls that contain no physical holes or foreign contaminants, the buyer halts payment and files formal claims against the roll supplier.
Customs inspectors reclassify contested yardage. If inspection logs declare rolls as second-quality scrap, import authorities scrutinize declared values, suspecting undervaluation to avoid customs tariffs. Conversely, providing raw, unverified optical inspection reports showing ten thousand defect counts creates export audit liabilities.
Proving that automated optical counters resolved multi-axial specular glares via cross-polarization and spatial filtering protects the supplier against punitive penalty clauses and claims for defective lot replacement.
Mill margins vanish under sustained clawbacks. A 40-tonne order of split bicomponent microfiber nonwoven represents nearly two hundred thousand dollars in trade value. Sourcing agreements require that automated roll defect logs attach cross-referenced visual validation records before invoicing.
When inspection software accurately filters specular refraction, scrap rates drop from eight percent down to 0.4 percent across monthly production runs. The resulting debit memo transfers the optical yield loss directly back to the spunbond vendor within thirty calendar days.