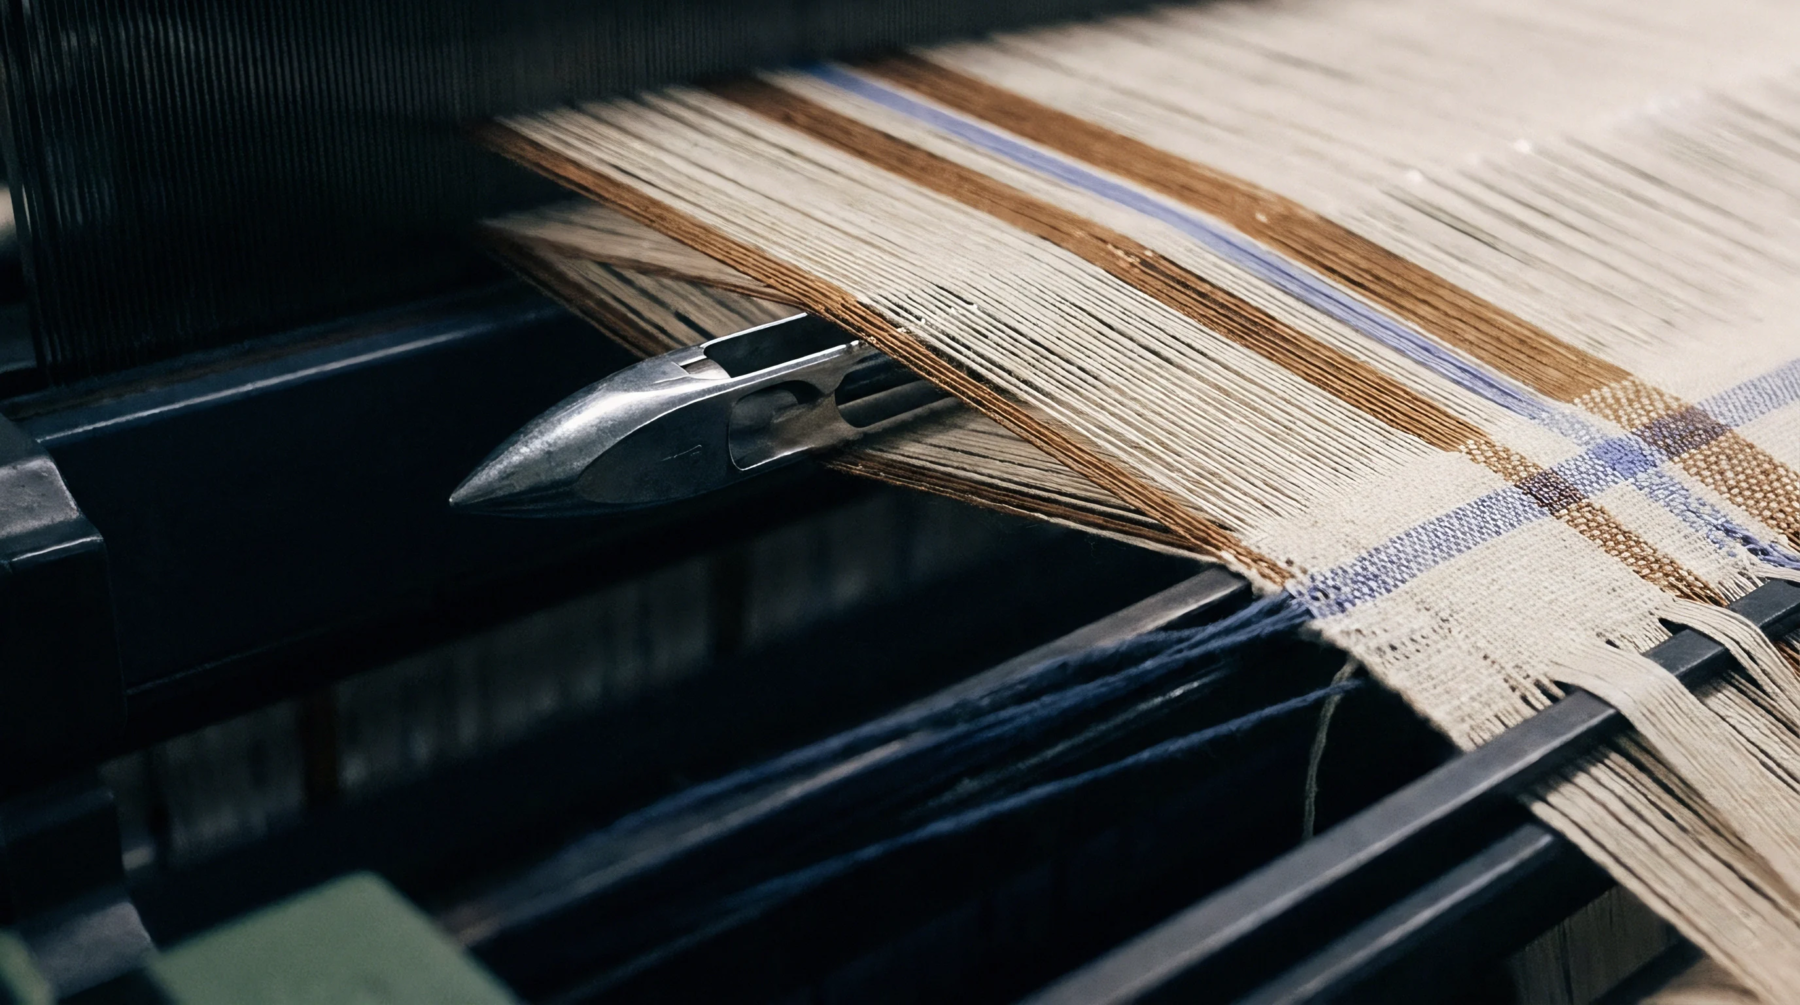
Basic Minimum Warp Set Calculation Principles for Greige Weaving
Greige warp set calculations must integrate reed width contraction, warp crimp, sizing stretch, and setup waste to establish accurate yarn purchase masses.
Production efficiency within weaving facilities relies upon the ratio of idle equipment time during warp or weft replenishment to the total potential capacity of active machinery across a standard work cycle. Calculating a loom changeover downtime rate quantifies the operational friction inherent in transitioning between different fabric styles, yarn counts, or color sequences on a single unit. This value excludes planned maintenance outages or mechanical breakdowns that occur during the actual production run of a stable fabric batch.
Facilities apply this metric to isolate the speed and effectiveness of manual interventions required to restart output after a material exhaustion event or a pattern change directive. Accuracy depends upon logging the exact moment a warp beam reaches its minimum clearance point and measuring the interval until the first pick of the subsequent roll hits the cloth fell.
Operators perform a sequence of physical tasks involving the removal of the depleted beam, the threading of new ends through the reed and heddles, and the tension calibration of the new warp. Skilled personnel reduce this duration by staging materials near the frame before the stop occurs. Standardized workflows ensure that heavy lift equipment stands ready to swap the harness frames without stalling the mechanical reset.
Every minute spent in this state subtracts from the possible revenue of the unit and increases the cost per meter of the final product. Variance in the mechanical complexity of the loom setup directly influences the total hours recorded for these stops. Complex dobby or jacquard heads require longer preparation than basic plain weave setups because the drawing-in process for thousands of individual warp ends remains a labor intensive procedure.
Managing high levels of loom changeover downtime rate forces mills to prioritize long production runs over smaller orders to reduce the frequency of machine stoppages. When this figure spikes, the mill experiences reduced throughput, which prevents the facility from fulfilling tight delivery schedules for urgent orders. High stoppage percentages signal a need for improved training for warp tiers or better preparation for the creeling area.
Production managers utilize this data point to determine the threshold for minimum order sizes, as small quantities drive the percentage upward and render the production cycle unprofitable. Consistency across the shop floor confirms that operators follow the defined procedures for beam mounting and knotting.
Measuring equipment throughput ignores the variance in yarn quality that causes incidental breaks, as the rate tracks only deliberate changes to the manufacturing process. External variables like humidity shifts in the weaving room or sudden power fluctuations do not enter the final calculation. Verification of this statistic occurs at the mill level through manual logs or digital sensors attached to the stop motion relays of the frame.
This accounting method serves as an objective measure of procedural speed that remains independent of the specific loom manufacturer or the type of fibre processed. Low values correlate with high equipment utilization, although excessive pressure to minimize this downtime occasionally results in improper tension settings that damage the warp ends.
Greige warp set calculations must integrate reed width contraction, warp crimp, sizing stretch, and setup waste to establish accurate yarn purchase masses.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.