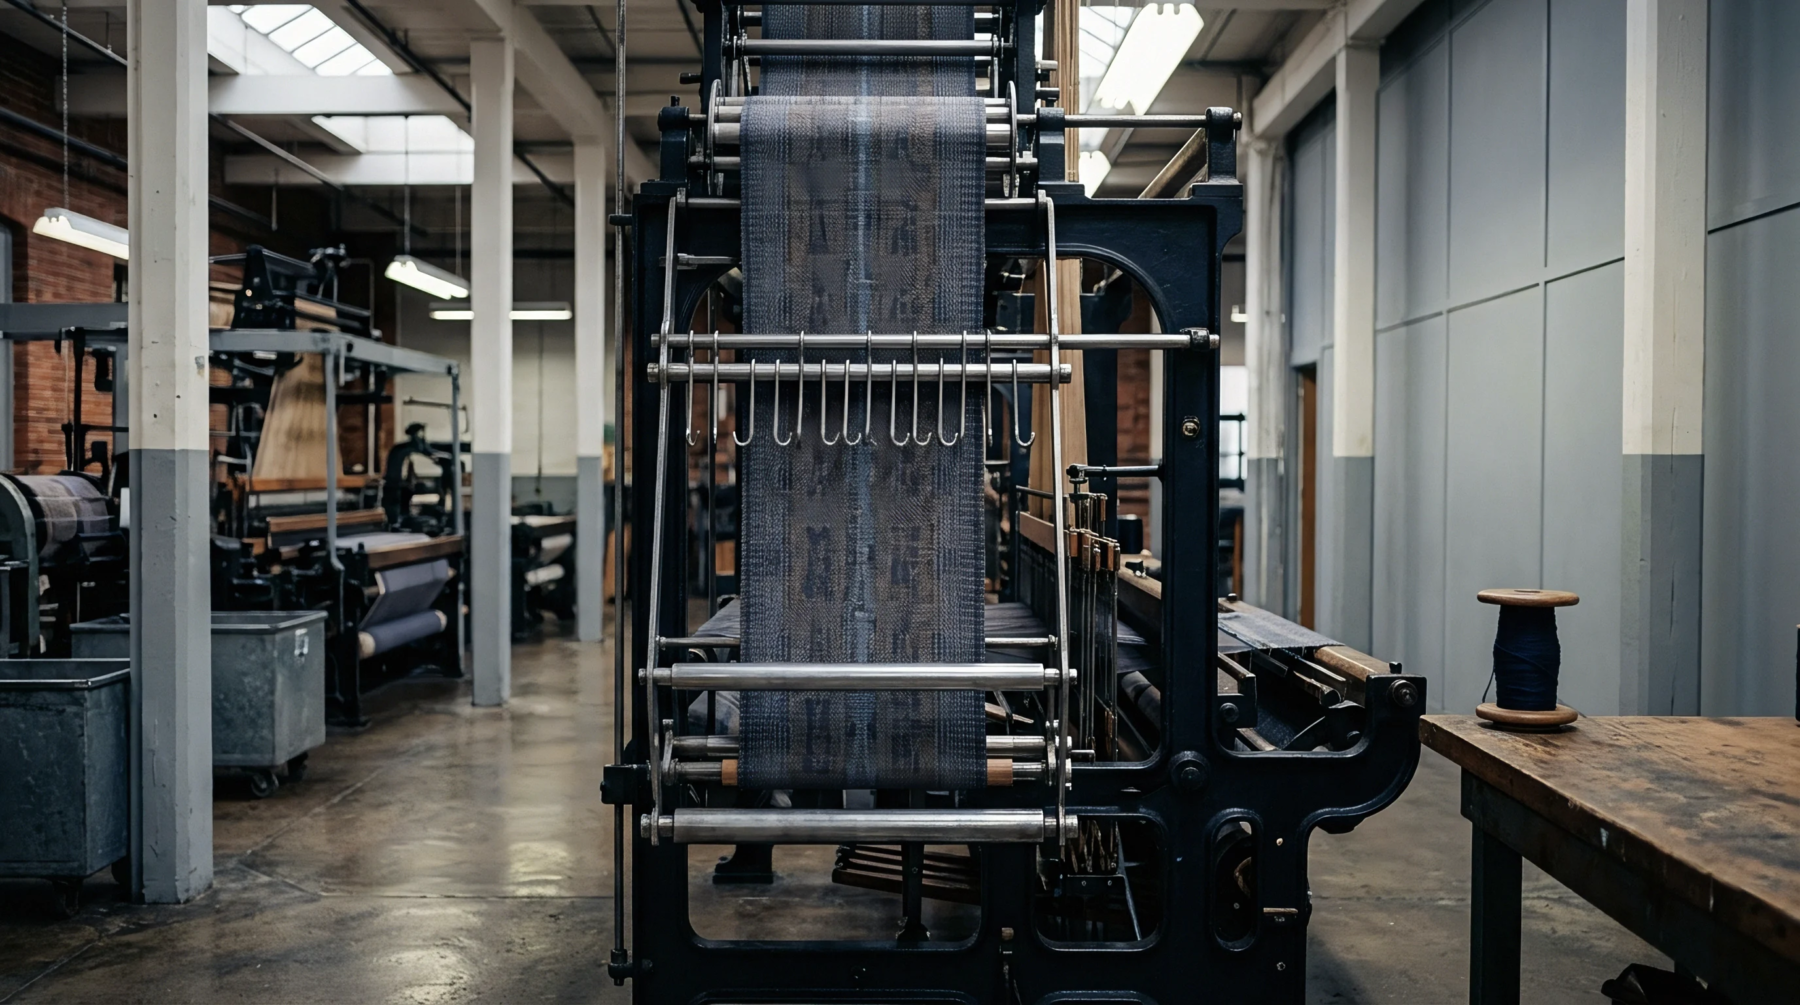
Fabrication System
Loom configurations engineered to form continuous woven structures exceeding standard apparel widths produce flat goods across operating spans from approximately two metres to well over five metres. Broad width weaving operates through reinforced rapier, projectile, or air-jet insertion mechanics designed to propel filling yarns across long shed openings without loss of trajectory or tension control. The technique supplies technical markets, geotextiles, wide drapery, and wide-format sheeting without longitudinal joining seams.
Structural demands increase nonlinearly as width expands, requiring rigid machine frames and counterbalanced sley assemblies to maintain uniform beat-up forces.
Mechanical Tension
Dynamic yarn management presents the chief technical hurdle across an expanded width. Warp sheets suffer tension differentials between the selvedge edges and the centre line, an imbalance caused by beam deflection, heald frame compliance, and variable yarn paths through the harness. Filling yarns experience extended dwell times in the shed, increasing susceptibility to aerodynamic decay in air-jet systems or projectile deceleration on mechanical carriers.
Accumulator feeders and precision tensioners compensate for these shifts to avoid filling loops and loose picks. Heavy beat-up pressures over several metres demand rigid reed supports to prevent center-sag and density drift across the piece.
Physical Deviation
Dimensional instability and mass variance often develop across the transversal profile of the greige goods. Broad fabrics tend to contract unevenly during wet processing, producing an hourglass effect or edge curl when selvedge tensions diverge from the ground structure. Pick density may drift from center to selvedge if the sley deflects during beat-up, causing visible bands or density gradations across the cut roll.
Distorted weft trajectories, commonly manifesting as bow and skew, worsen with broader widths and require active multi-roller optical weft straighteners on the finishing range.
Inspection Tolerance
Commercial acceptance relies on cross-width density consistency verified by cut-and-weigh sampling and pick counting at the left, centre, and right zones of the bolt. Width deviations are held within contract margins, typically negative zero to plus two percent of nominal measure. On-loom optical scanning systems monitor warp yarn breakage, flagging mispicks and end outs before extensive yardage accumulates.
Finished lots undergo tensile and burst testing across the entire width profile to establish that edge zones maintain the structural integrity verified at the core of the roll.