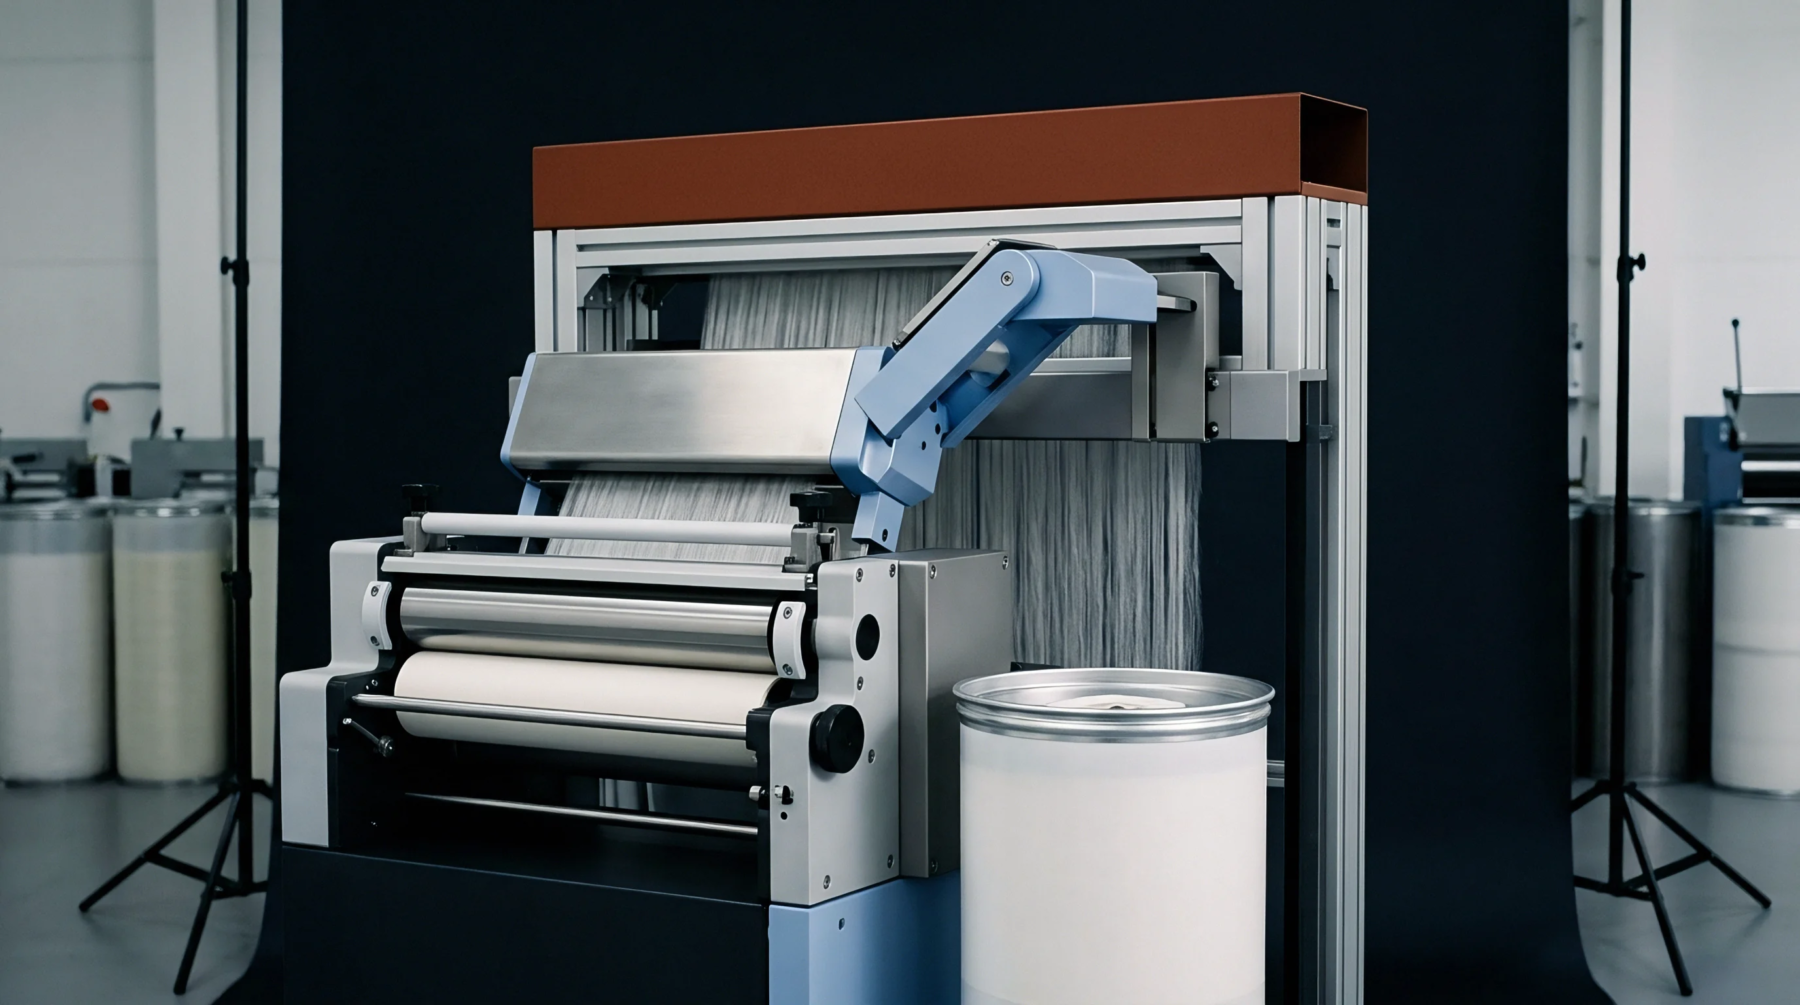
Greige Warp Beaming Economics and Basic Minimum Calculation
Greige warp beaming economics requires minimum 5000 metre set lengths to absorb fixed slasher setup losses, sizing waste, and creel remnant expenses.
A specific total quantity of linear footage calculated for a single warping operation provides the exact warp demand for the production run of a given fabric quality. The loom set length dictates the quantity of yarn wound onto the warp beam before the processing of the textile begins. Production planners determine this figure by multiplying the total number of pieces scheduled for the run by the standard unit length plus any necessary waste allowance for sampling or machine tensioning.
Accurate calculation prevents the interruption of the weaving process because the supply of warp yarn matches the output requirements of the loom. Underestimating this figure forces a stoppage to reload the warp beam whereas overestimating leads to leftover yarn that cannot move to a different style. Machines require consistent tension across the full duration of the cycle to avoid defects in the fabric structure.
Managers verify the integrity of the total yardage by comparing the planned warp length against the actual beam capacity and the length per piece. Each beam has a fixed physical limit dictated by the flange diameter and the width of the yarn sheet. When the demand exceeds the mechanical capacity of one beam the production team must split the order into smaller segments or install a larger beam if the loom dimensions permit such adjustments.
Proper calculation considers the shrinkage factors that occur during subsequent finishing stages because the fabric dimensions alter once the tension releases after the loom stage. Practitioners look for the correlation between the raw material inventory and the final output to ensure the efficiency of the mill floor. If the calculation fails to account for the take up during weaving the final fabric pieces often fall short of the required sellable length.
Warehouse staff manage the raw material stock by aligning the physical count of yarn cones with the planned length per beam. Each set of cones must supply sufficient yardage to cover the beam requirement plus the tailing waste that inevitably remains after the last piece clears the reed. Procurement teams track these requirements over multiple production cycles to refine the waste factors assigned to different fibre types.
Filament yarns often require less buffer than spun yarns because breakage rates differ across material properties. The inventory remains accurate when the actual consumption data feeds back into the planning software to adjust future sets.
Mechanical constraints during the winding process determine the quality of the final warp. Consistent speed and tension control during the preparation of the beam prevent variations in the density of the yarn sheet. High tension leads to excessive stretch in the warp while low tension creates slack zones that trigger stop motions on the loom.
A correctly calibrated machine ensures that the yarn tension stays within a narrow range throughout the entire length of the beam. Uniform winding produces superior fabric quality.
Greige warp beaming economics requires minimum 5000 metre set lengths to absorb fixed slasher setup losses, sizing waste, and creel remnant expenses.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.