Jet Dye Liquor Flow Resistance in Swollen Cotton Twill Fabrics
Swollen cotton twill fibers restrict jet dye liquor flow by reducing void volume, requiring calibrated nozzle diameters and lower pump pressures to prevent unlevelness.
Impedance
Cellulose fiber water absorption transforms the internal void geometry of heavy woven cotton during aqueous wet processing. When dry cotton twill fabric enters an aqueous bath inside a jet dyeing machine, liquid molecules penetrate the amorphous regions of the cell wall. Hydrogen bonding between water molecules and hydroxyl groups on the cellulose polymer chains forces the primary microfibrils apart.
This molecular displacement causes significant dimensional alterations at the yarn and fabric levels, altering the hydrodynamic behavior of the running rope inside the jet tube.
Pores shrink rapidly.
The volumetric expansion of individual cotton fibers occurs asymmetric to the fiber axis. Diameter expansion ranges between fourteen and twenty-two percent, while axial length increases by less than two percent. As yarn cross-sections swell within the locked geometry of a woven twill structure, the inter-fiber spaces inside the yarn bundles compress.
Simultaneously, inter-yarn voids between warp and weft threads constrict as yarn diameters grow. This dual-level pore reduction drastically increases fluid friction, restricting bulk liquor transport through the fabric substrate.
Hydraulic Permeability in Hydrophilic Woven Matrices
Darcy’s law governs low-velocity fluid passage through untangled textile structures, relating volume flow to applied hydrostatic differential. The basic relationship defines superficial velocity through a porous bed based on fluid viscosity, sample thickness, and the intrinsic permeability coefficient of the material. In a dry or relaxed cotton twill, high macro-porosity permits rapid fluid dissipation under low pump pressures.
Once wetting and fiber expansion initiate, the intrinsic permeability coefficient drops by up to two orders of magnitude.
Fluid shear increases friction.
Liquor movement through a jet dyeing machine relies on both kinetic transport down the jet pipe and forced penetration through the folded fabric rope. Hydrodynamic resistance inside swollen twill fabrics converts mechanical pump energy into localized hydraulic drag. When liquor flow resistance rises, the differential pressure across the fabric rope increases.
If the circulation pump cannot sustain the required pressure gradient, fluid bypasses the dense interior of the rope, traveling almost exclusively along the outer fabric folds.
| Process Stage | Mean Pore Radius (um) | Fabic Void Fraction (%) | Permeability (10^-12 m2) | Pressure Drop (kPa/m) |
|---|---|---|---|---|
| Dry Greige State | 42.5 | 0.48 | 18.4 | 12.1 |
| Scoured Cold Wetting | 28.1 | 0.31 | 6.2 | 38.5 |
| Caustic Swollen (80C) | 11.4 | 0.16 | 0.8 | 184.2 |
| Post-Fixation Bleached | 18.6 | 0.22 | 2.1 | 96.7 |
Volumetric Fiber Swelling Mechanics
Cotton crystalline microfibrils absorb water and polar solvents, driving a lateral diameter increase between fourteen and twenty-two percent while longitudinal expansion remains below one percent. Alkali additions during reactive dyeing exacerbate this dimensional shift. Sodium hydroxide or sodium carbonate dosing raises the osmotic pressure inside the fiber, forcing additional water molecules into the cell wall.
The swollen fibers expand into the interstitial spaces of the yarn, converting open flow channels into narrow capillary paths.
Cell walls expand sideways.
A twenty percent fiber diameter swell reduces interstitial fabric permeability by seventy-four percent under standard aqueous jet dyeing liquor flow rates.
The structural geometry of twill weaving intensifies fluid blockage compared to plain weaves of identical mass. Twill constructions feature long yarn floats and dense packing arrangements, such as 2/1 or 3/1 weave architectures. When yarns expand in a high-density 3/1 twill, the overlapping float segments press tightly against adjacent yarns.
This mechanical contact seals the diagonal twill ridges, creating a continuous barrier against transverse liquor flow during jet circulation.
Ignoring hydraulic permeability loss during cotton fiber swelling leads directly to core starvation, shade streaking, and costly dye lot rejections.
Pack
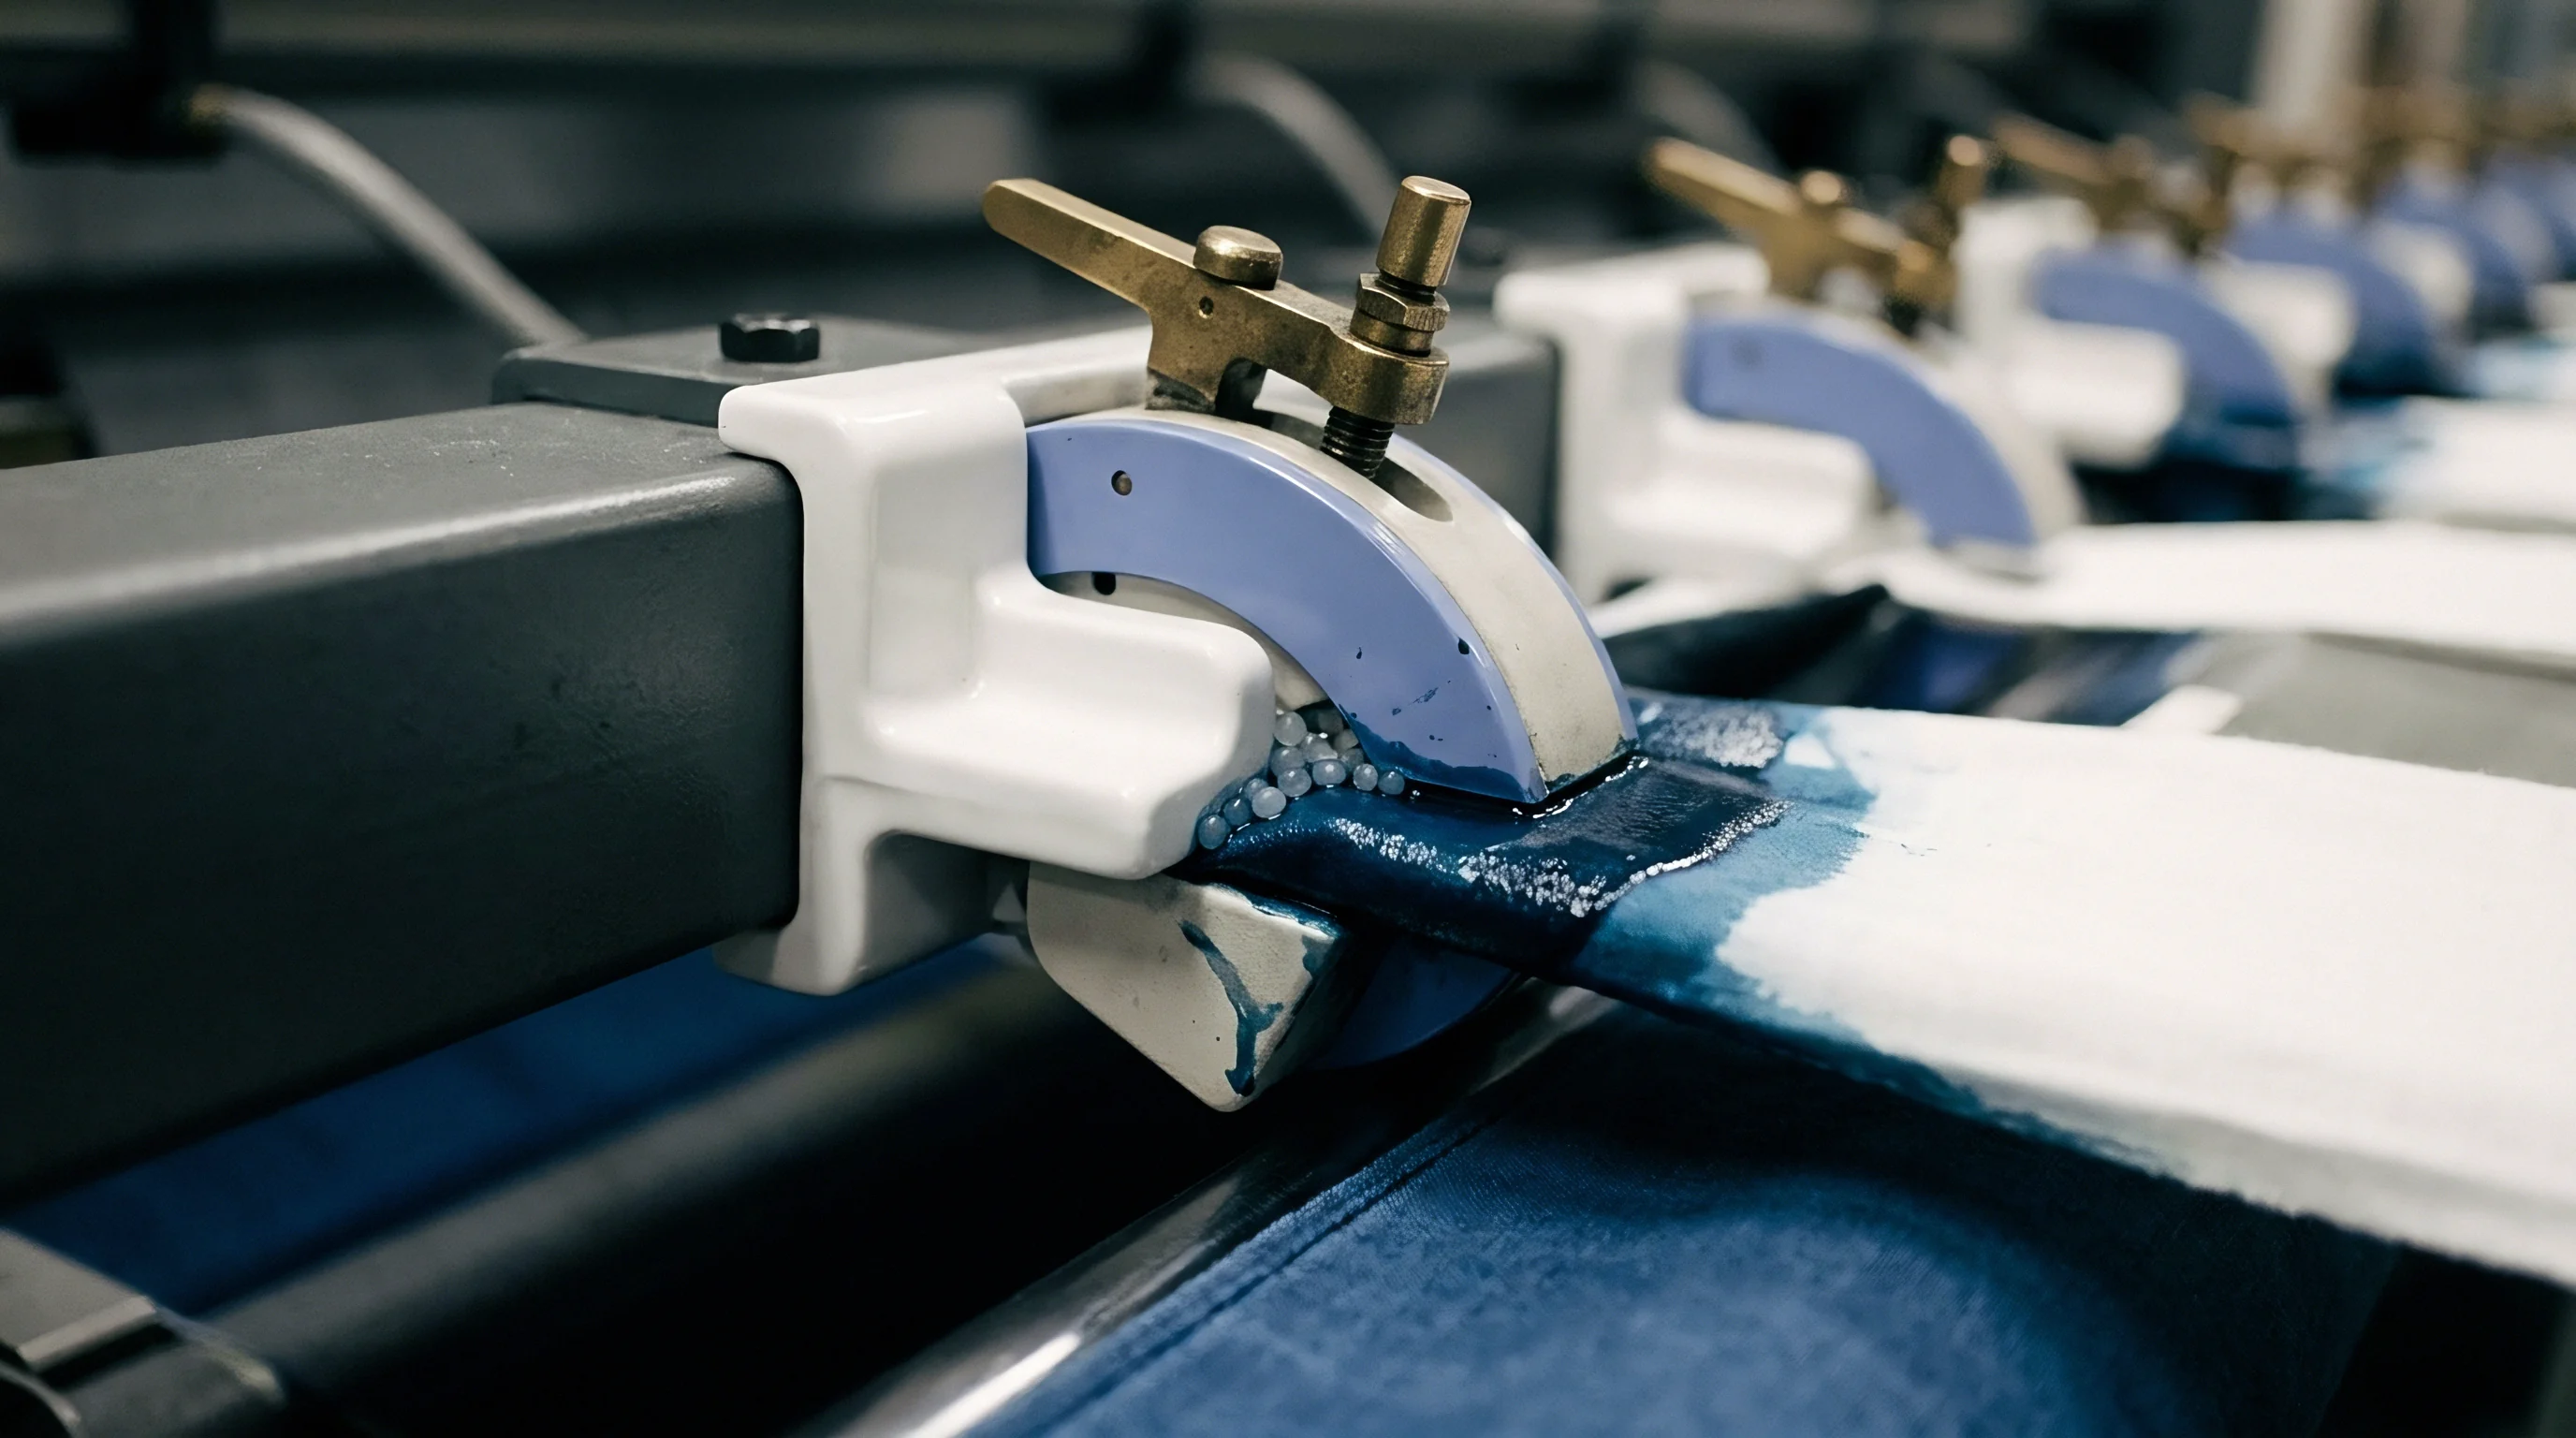
Rope compaction inside jet dyeing machine transport tubes restricts liquor circulation channels during high-velocity machine cycles. As the fabric rope travels through the Venturi nozzle and drops into the main storage chamber, gravitational packing compresses the wet cloth into a dense mass. The mechanical weight of the wet fabric column drives liquid out of the internal void spaces, producing a compacted structure with minimal inter-rope permeability.
Compact ropes resist liquor.
Liquor transport through this packed fabric mass depends entirely on the mechanical pressure head generated by the main circulation pump. As the fabric rope densifies under its own submerged weight, the force necessary to drive dye liquor through the core of the rope escalates rapidly. Insufficient liquor force causes the circulation fluid to flow around the exterior of the fabric bundle, leaving the internal core starved of fresh dye chemistry and dissolved alkalis.
Kozeny-Carman Void Fraction Modification
The hydraulic pore radius shrinks non-linearly as cell walls enlarge, causing the interstitial void fraction to drop from an initial dry baseline near forty percent down below eighteen percent. The Kozeny-Carman equation models this hydrodynamic restriction by treating the packed fabric rope as a bundle of capillary tubes with a specified tortuosity factor. Swelling increases both the specific surface area of the fibers and the tortuosity of the fluid path through the fabric matrix.
Crimp increases flow drag.
Mathematical representation of the Kozeny-Carman relationship highlights the extreme sensitivity of flow resistance to changes in void fraction. The hydraulic resistance parameter varies inversely with the cube of the fabric porosity. Consequently, a small reduction in fabric void volume due to cotton fiber swelling generates a massive increase in pressure drop across the fabric rope.
In heavy twill fabrics exceeding 250 grams per square meter, this mathematical relationship explains why minor adjustments in processing temperature or electrolyte concentration cause sudden operational failures.
Which Jet Nozzle Parameters Minimize Swollen Rope Compression?
Venturi nozzle throat geometry dictates both physical transport force and mechanical constriction exerted on the wet fabric rope. Selecting a nozzle diameter that is too narrow for a swollen heavy twill forces the fabric through an aggressive mechanical pinch point. This mechanical compression squeezes out interstitial liquor right at the point where high-velocity liquor injection ought to penetrate the cloth core.
Oversized nozzles reduce transport velocity, leading to rope stoppage and severe crease formation.
Slower rope turnover speeds in dense cotton fabrics create localized temperature gradients that worsen reactive dye unlevelness.
Optimal nozzle performance requires balancing hydraulic driving pressure against physical throat clearance. A variable-gap Venturi nozzle allows technicians to adjust the internal cross-sectional clearance while maintaining constant volumetric fluid flow. Lowering the physical compression on the swollen rope preserves a higher internal void fraction, facilitating liquor penetration during the high-velocity jet transition phase.
- Channeling Defect occurs when dye liquor bypasses compressed rope cores, producing longitudinal pale streaks along internal fabric folds.
- Rope Stop Jamming develops when excessive flow resistance reduces rope buoyancy, causing fabric accumulation in the storage chamber.
- Chafing Abrasion arises from high differential speed between the driving liquor stream and the slowed fabric rope inside the nozzle throat.
- Crease Mark Retention results from prolonged static compaction of swollen fibers at high temperatures without sufficient liquor cushioning.
Equipment suppliers frequently contend that severe rope compaction and unlevel shade results stem entirely from poor wetting agent dosing rather than inadequate nozzle aperture sizing.
Anisotropy
Twill weave geometry creates asymmetrical flow paths along warp and weft directions due to floating yarn structures and directional alignment. Unlike plain weave fabrics where warp and weft intersections form a uniform square grid, twill fabrics feature diagonal float lines that offer paths of lower hydraulic resistance. Fluid moving parallel to the twill line experiences lower friction than fluid attempting to pass perpendicular to the diagonal ridges.
Warp floats ease longitudinal flow.
This structural anisotropy causes non-uniform dye liquor dispersion through the thickness of the fabric. In a 3/1 right-hand twill, liquor injected under pressure tends to slide along the surface warp floats rather than penetrating straight through the fabric body. As cotton fibers swell, the gap between parallel float yarns closes faster than the gap at yarn intersections, amplifying the directional flow discrepancy.
Floating Thread Structural Bias
Diagonal weave lines of two-up one-down or three-up one-down constructions leave prominent surface float segments that guide fluid movement along preferred channels. Fluid dynamics dictates that liquid follows the path of least mechanical resistance. Surface floats create continuous open micro-channels along the diagonal angle of the weave.
Under forced jet circulation, liquor channels along these surface tracks, bypassing the tightly bound yarn crowns beneath.
High velocity creates channel flow.
Directional permeability measurement reveals distinct coefficients for warp-wise, weft-wise, and through-thickness fluid vectors. Through-thickness permeability in heavy cotton twill drops faster during fiber swelling than directional surface permeability. This anisotropy ratio imbalance forces dye liquor to travel across the fabric face rather than through its depth, creating core-to-surface dye concentration gradients.
| Weave Structure | Warp Float (mm) | Warp Permeability (m2) | Weft Permeability (m2) | Anisotropy Index |
|---|---|---|---|---|
| 2/1 Warp Twill | 1.2 | 4.1 x 10^-12 | 2.8 x 10^-12 | 1.46 |
| 3/1 Warp Twill | 1.8 | 6.8 x 10^-12 | 3.1 x 10^-12 | 2.19 |
| 2/2 Broken Twill | 0.9 | 3.2 x 10^-12 | 3.0 x 10^-12 | 1.07 |
| 4/1 Satin Twill | 2.5 | 9.4 x 10^-12 | 3.4 x 10^-12 | 2.76 |
Warp and Weft Thread Density Interdependence
High pick counts restrict transverse liquor penetration far more aggressively than equivalent warp end densities because pick insertion locks the crimp configuration into place. In heavy workwear twills, warp density frequently exceeds forty ends per centimeter, while weft density sits between twenty and twenty-six picks per centimeter. The tight packing of warp threads creates high lateral flow resistance across the warp sheet.
Tight picks block fluid.
Under ISO 105-J03 color difference evaluations, internal yarn core shade variance across a dense twill rope stays below 0.6 DE00 to pass automotive trim specifications.
When the fabric undergoes mechanical tension during jet transport, warp threads straighten, transferring crimp onto the weft yarns. The increased weft crimp amplifies weft yarn cross-sectional flattening, further sealing inter-yarn pores. This dynamic structural modification during circulation means that flow resistance changes continuously as the fabric transitions between high-tension nozzle zones and low-tension storage zones.
Wider float lengths in twill weaves always ease longitudinal fluid movement while increasing the risk of transverse liquor channeling.
Differential
Pressure drop across the fabric rope wall increases exponentially as fluid velocity scales up during rapid circulation cycles. Fluid dynamic equations show that pressure loss in laminar regimes scales linearly with velocity, but transitions to quadratic scaling once turbulent micro-eddies form around structural yarn crowns. Inside swollen cotton twill, the internal pore channels are small enough to force flow into high-shear micro-viscous regimes, elevating static pressure differentials across the rope bundle.
Nozzle constriction raises pressure.
High differential pressure forces fluid through low-resistance pathways, leaving high-density zones under-serviced. When the pressure differential across a fabric fold exceeds the mechanical resistance of the surrounding rope mass, the liquor ruptures through the fold edge, creating localized fluid jetting. This localized jetting washes unfixed dye away from specific areas, leading to pale streaks and uneven color yield.
Circulation Pump Head Pressure Dynamics
Centrifugal pumps delivering dyeing liquor must overcome both static pipe resistance and the dynamic hydraulic barrier created by compressed wet cotton. Pump performance curves indicate a sharp drop in delivered volumetric flow rate as system backpressure rises. When a swollen twill fabric rope enters the jet transport tube, backpressure climbs, moving the pump operational point toward its shut-off head zone.
Pump head loss escalates.
Operating near shut-off head reduces total liquor flow rate, extending the time required for a complete bath turnover. In reactive dyeing, slow bath turnover allows dye molecules to hydrolyze in the aqueous solution before penetrating the swollen core of the yarn bundles. Ensuring sufficient pump capacity requires selecting impellers designed to deliver stable volumetric output against variable hydraulic resistance loads.
Liquor-to-Goods Ratio Impact on Penetration Resistance
Bath volumes set below five to one force concentrated chemical distribution through tight yarn intersections, elevating fluid shear stress. Ultra-low liquor ratios decrease the available hydraulic driving head outside the fabric rope while increasing the concentration of dissolved salts and alkalis. Electrolytes promote rapid cellulose swelling, triggering early hydraulic pore closure before level dye migration completes.
Lower liquor ratios increase drag.
Higher liquor ratios provide additional fluid volume that acts as a mechanical lubricant and thermal damper inside the storage chamber. The increased total mass of the bath assists in opening fabric folds, preventing persistent channeling paths. However, excess liquor volume increases water consumption, thermal energy demands, and chemical requirements, creating a direct conflict between processing costs and dyeing quality.
Higher pump speed cannot overcome severe pore closure in heavily swollen cotton twill without increasing fabric rope chafing.
- Evaluate Greige Void Fraction by measuring dry fabric density, yarn crimp, and fiber cross-sectional area prior to dye lot loading.
- Calculate Swollen Hydraulic Resistance using modified Kozeny-Carman parameters adjusted for target processing temperature and electrolyte concentrations.
- Select Nozzle Aperture Clearance to match maximum expected swollen rope volume, avoiding physical rope pinch during high-speed circulation.
- Modulate Circulation Pump Velocity to maintain constant differential head without exceeding maximum allowable fabric surface shear limits.
Standard purchasing agreements under ISO 105-X12 specify that bulk dye lots displaying edge-to-center shade variances greater than grade 4-5 incur immediate financial chargebacks.
Diagnostics
Quantifying hydraulic drag inside closed pressure vessels requires specialized sensor arrays and differential pressure transmitters across the jet nozzle assembly. Real-time measurement of fluid pressure drops provides dyehouse technicians with immediate feedback regarding fabric permeability modifications during the heating and dosing phases of the dye cycle.
Wet twill collapses under pressure.
Without accurate diagnostic instrumentation, operator adjustments rely on subjective observation of rope circulation speed. Monitoring differential pressure trends allows automated control systems to adjust pump frequency drives dynamically. This automated response prevents sudden backpressure spikes caused by rapid alkali-induced fiber swelling.
Differential Transducer Placement Protocols
Piezoresistive pressure sensors installed immediately before and after the Venturi throat capture the precise head loss generated by wet fabric passage. Sensor taps must be positioned flush with the internal pipe wall to prevent fluid turbulence from distorting static pressure readings. High-frequency signal sampling filters out pressure pulses generated by circulation pump impeller blades.
Core penetration demands time.
Analyzing differential pressure signal noise reveals physical rope performance inside the jet tube. Uniform pressure traces indicate smooth rope movement with consistent liquor penetration. Erratic, high-amplitude pressure spikes signal periodic rope jamming, fold collapse, or severe localized liquor blockage inside swollen fabric zones.
Worked Hydraulic Resistance Calculation
Assume a 300 kg batch of 3/1 cotton twill fabric running in a single-tube jet machine at a liquor ratio of six to one. The dry fabric weight is 280 grams per square meter, with an initial porosity of 0.42. Upon heating to 60C and dosing sodium carbonate, cellulose fiber diameter swells by eighteen percent, dropping calculated fabric porosity to 0.19.
The specific surface area of the yarn matrix increases from 1.8 x 10^5 m^-1 to 2.4 x 10^5 m^-1 due to microfibrillar dispersion.
Applying the Kozeny-Carman relationship under these specific process parameters yields the following hydraulic transformation:
Dry state permeability K_1 = (0.42^3) / (5 (1 – 0.42)^2 (1.8 x 10^5)^2) = 1.36 x 10^-11 m2.
Swollen state permeability K_2 = (0.19^3) / (5 (1 – 0.19)^2 (2.4 x 10^5)^2) = 3.65 x 10^-13 m2.
The calculation demonstrates a 37-fold decrease in intrinsic fabric permeability. To maintain a constant flow velocity of 1.5 meters per second through the fabric rope under these swollen conditions, the required differential driving pressure across the nozzle throat scales from 14.2 kPa up to 525.4 kPa. Because the machine circulation pump cannot exceed a maximum head capacity of 220 kPa, actual liquor flow velocity drops to 0.62 meters per second, causing a severe reduction in rope circulation turnover frequency.
Measuring fluid resistance through wet fabric involves the following sequential execution steps:
- Isolate differential pressure sensing lines by flushing entrained air bubbles with deaerated water.
- Record baseline pressure drop across the empty nozzle throat at target volumetric flow rates.
- Load fabric sample and run cold water circulation cycle to establish initial wet unswollen pressure drop.
- Inject salt and alkali dosing solutions while recording continuous pressure differential vs time curves.
Whether real-time differential pressure telemetry can dynamically modulate pump drive speed fast enough to prevent rope creasing in heavy twills remains an open question for dyehouse automation engineers.
Friction
Boundary layer resistance between moving dye liquor and swelling yarn surfaces governs energy dissipation and level dye strike. Fluid moving past stationary cellulose microfibrils experiences drag caused by viscous shear forces within the boundary layer. As the fiber surfaces swell and become hydrophilic, bound water layers form on the microfibril edges, increasing physical wall roughness at the sub-micron scale.
This increased microscopic wall roughness thickens the laminar boundary layer, restricting mass transfer of dye molecules from the bulk liquor into the fiber interior. Elevating dye bath temperatures reduces bulk fluid viscosity, but simultaneously accelerates reactive dye strike rates. If boundary layer drag remains high while strike rates accelerate, dye molecules deplete rapidly at the outer fiber boundaries, worsening cross-sectional shade ring-dyeing defects.
Surface Lubricants and Penetration Auxiliaries
Non-foaming fatty acid ester surfactants lower surface tension, accelerating core wetting and reducing boundary layer drag during cold pretreatment and hot dyeing stages. Wetting agents lower the contact angle between the aqueous dye liquor and the hydrophobic wax remnants on unbleached cotton fibers. This surface action facilitates rapid liquid entry into micro-capillaries before fiber swelling completely seals the inter-yarn voids.
Polymeric friction reducers act as internal lubricants between individual fabric folds. These high-molecular-weight additives modify the rheological properties of the boundary layer, inducing shear-thinning behavior under high flow velocity. Lowering dynamic friction at the fiber-liquor interface allows dye liquor to penetrate compressed fabric rope cores with significantly reduced pressure head requirements.
| Nozzle Size (mm) | Pump Speed (RPM) | Pressure Drop (bar) | Flow Rate (L/min) | Energy (kWh/kg) |
|---|---|---|---|---|
| 120 | 1450 | 0.85 | 420 | 0.38 |
| 100 | 1450 | 1.62 | 310 | 0.52 |
| 80 | 1780 | 2.85 | 220 | 0.89 |
| 140 (Variable) | 1200 | 0.42 | 510 | 0.29 |
Optimizing jet dyeing performance for heavy, swollen cotton twill fabrics demands balance between fluid dynamics, chemical dosing profiles, and mechanical machine settings. Dyehouses must balance pump power delivery against internal fabric permeability limits to prevent core starvation, channeling, and rope creasing defects. Systemic adjustment of surfactant concentration alongside controlled heating ramps maintains liquor mobility through swollen twill structures until dye fixation completes.