Sampling Plans for Woven Coated Fabric Verification
Verifying woven coated fabrics demands combining ASTM D5430 visual grading with ISO 2859-1 statistical sampling and strict composite dilution limits.
Verifying woven coated fabrics demands combining ASTM D5430 visual grading with ISO 2859-1 statistical sampling and strict composite dilution limits.
Repeat textile orders demand digital tolerance baselines, dynamic sampling intensity shifts, and batch-level chemical verification rather than physical samples.
Dynamic creel stretch variability stems from unequal yarn path lengths and friction points, producing permanent polymer draw and irreversible dyehouse barre.
Verify raw fabric thread counts, sizing content, and four-point defect scores before wet processing to prevent irreversible dyeing failures and financial loss.
Commission textile contracts balance property risks and finishing specifications by linking bailed greige inventories directly to standardized lab test tolerances.
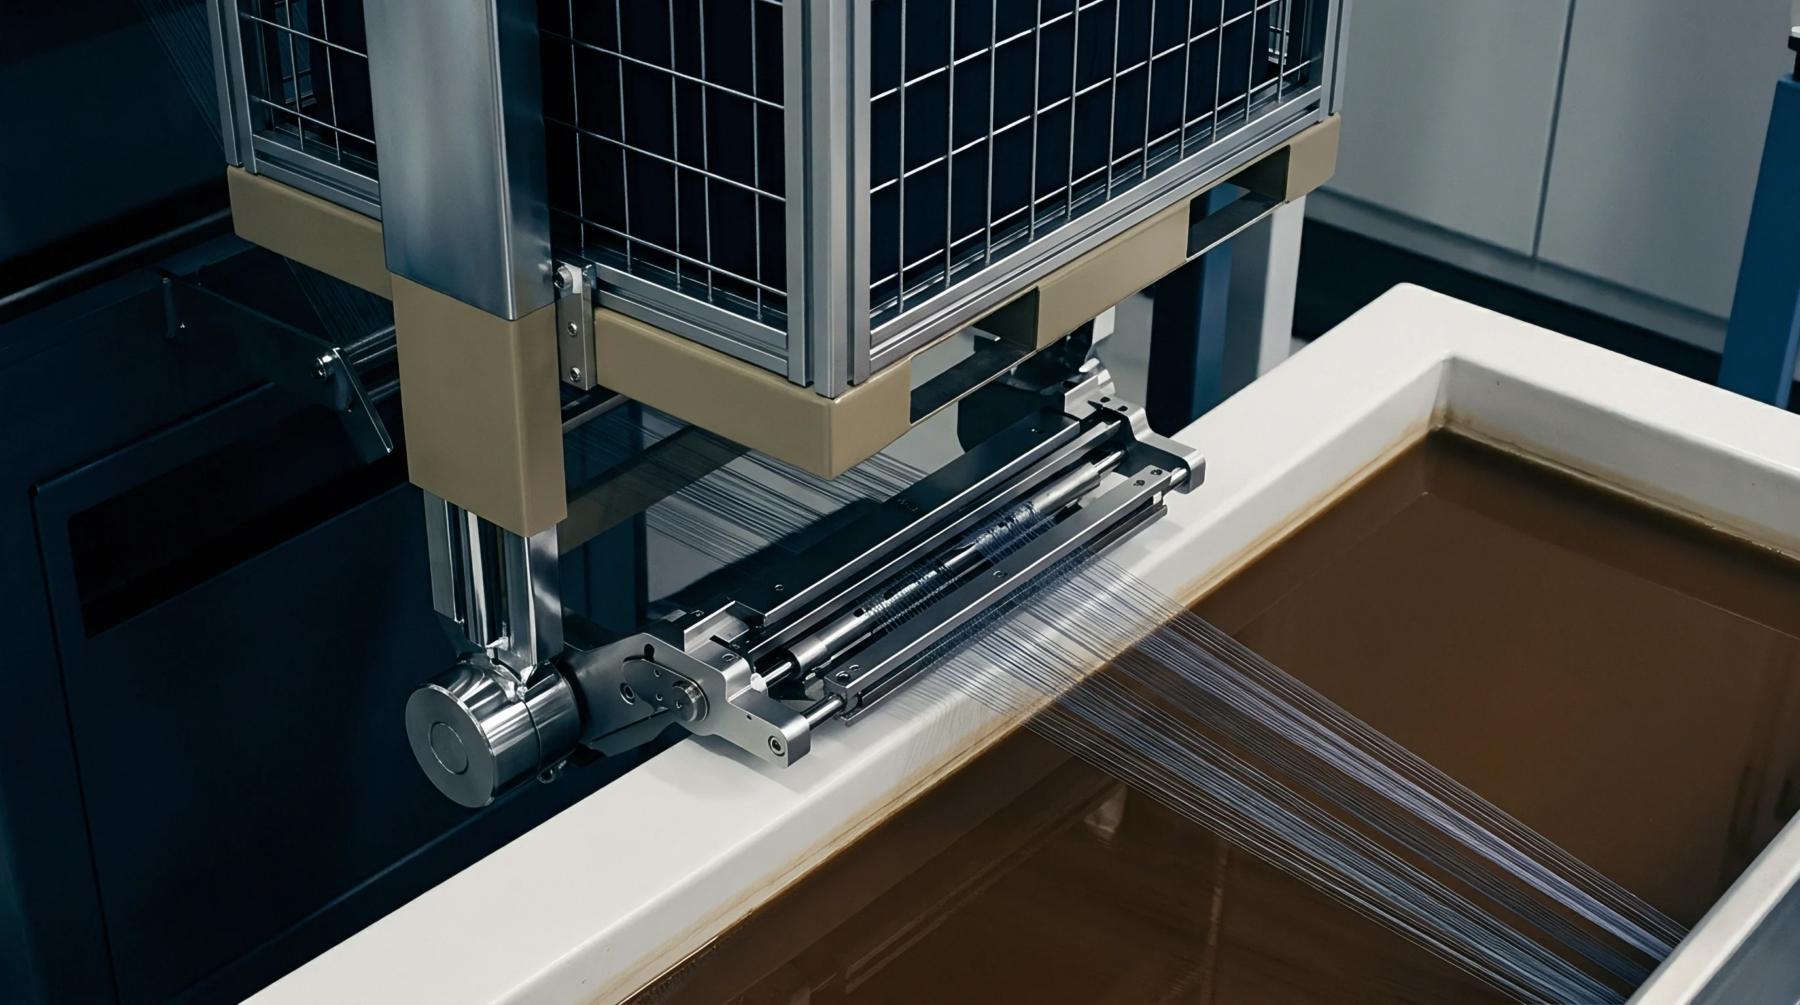
Continuous dyeing eclipses exhaust jet processing on direct manufacturing cost once run lengths surpass 3,200 finished metres for mid-weight woven twills.
Quantifying hydrophobic film defect frequency in combed knits combines ISO 811 hydrostatic testing with inline 0.1-millimetre optical scanning per 100 square metres.
Audit scopes must encompass spinning inputs through subcontract finishing lines to hold prime vendors liable for latent wet processing defects.
Dynamic yarn cross-sectional flattening expands major axis boundaries, defining absolute physical weaving limits and preventing bulk loom jamming failures.
Verify woven fabric density on conditioned finished goods using ASTM D3775 or ISO 7211-2 to catch off-loom overfeed tricks and protect garment seam strength.
Acceptance sampling for coated textiles pairs ASTM D5430 visual classification with ANSI/ASQ Z1.9 variables plans for destructive barrier verification.
Greige qualification governs wet processing uptake through conditioned mass accounting, chemical size identification, capillary absorbency, and bow tolerances.
Fabric performance depends on greige interlacing geometry, wet processing relaxation, and multi-mill supply chain lead times.
Fabric weight tolerance written as a mill range holds commercial validity only when tested under ISO 139 standard atmosphere using ISO 3801 methods.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.