Resolving Microscopic Scale Loss in Mechanically Recycled Animal Hair and Wool Blends
Resolving microscopic scale loss in recycled animal hair requires high-tenacity carrier wool additions and proteomic mass spectrometry verification.
Resolving microscopic scale loss in recycled animal hair requires high-tenacity carrier wool additions and proteomic mass spectrometry verification.
Lifting comber noil extraction from 10 to 18 percent raises Martindale abrasion by up to 80 percent, after which returns diminish against escalating fibre costs.
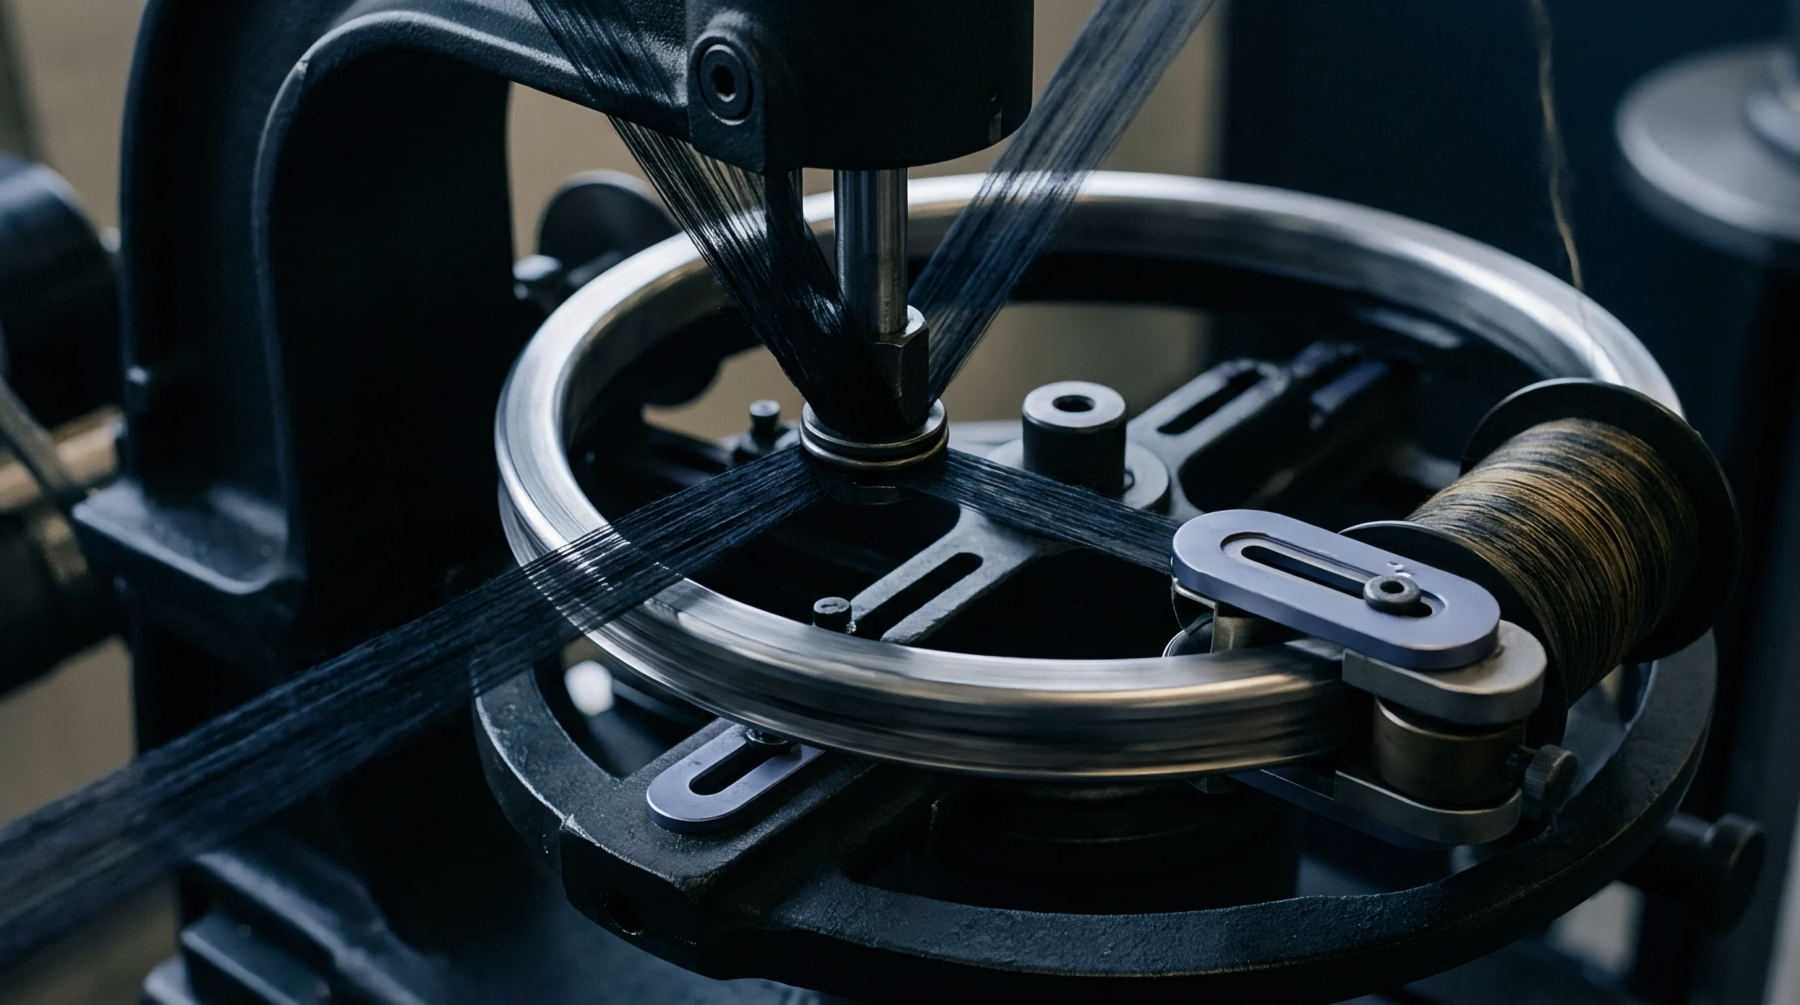
Managing yarn twist equilibrium requires steam autoclaving lively packages or alternating S/Z feeds to eliminate loop skew and cutting waste in single jersey fabric.
Plied yarns neutralize torsional spirality within the strand cross-section, while alternate feeds distribute opposed stresses across alternating courses.
Single jersey spirality is controlled by capping yarn twist multiplier below 3.5, optimizing loop tightness, and autoclaving to neutralize torsional torque.
Dense yarn acid retention drives core cellulose hydrolysis during drying; verification demands titratable acidity testing over surface pH averages.
Single fiber length skewness dictates carded ring spun tenacity by governing floating fiber drafting waves and ineffective stress transfer lengths.
Continuous wet processing of cotton yarns demands precise control of yarn structure, swelling draft, liquor application, and transport tension to assure performance.
Exceeding 3.5 elastane draft without heat-setting crosslinking causes sheath slip under prolonged static load.
Combing long-staple cotton to eighteen percent noil suppresses short fibers below six percent, locking ends into yarn cores to secure Grade 4 pilling life.
Warp cover factor calculation requires precise yarn diameter, density, and count conversions to establish enforceable fabric specifications and prevent bulk weaving defects.
Combing cotton sliver below 5.5% short fiber content raises rotor yarn tenacity ceilings to 18.5 cN/tex by reducing friction slip inside the rotor groove.
Optimize cotton staple selection by matching upper half mean length and short fiber index to target yarn counts to prevent drafting defects and lower landed yarn costs.
Yarn ply twist multiplier controls intra-bundle pore radius; multipliers above 4.0 cause surface ring-dyeing frosting while values under 3.2 provoke migration.
High-twist plied yarn core shade levelness requires metered alkali dosing to suppress Damköhler numbers below unity during early reactive dye migration.
Fabric performance depends on greige interlacing geometry, wet processing relaxation, and multi-mill supply chain lead times.
65/35 poly-cotton workwear performance relies on ring twist multipliers near 4.4 and early shed timing to maximize warp cover factor without pilling failure.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.