Minimum Colour Quantity Deciding a Range Plan before Design Does
Minimum colour quantities set dye vessel efficiency and enforce range plan fabric allocations long before garment sketches reach the pattern desk.
Minimum colour quantities set dye vessel efficiency and enforce range plan fabric allocations long before garment sketches reach the pattern desk.
Aligning woven greige warp minimums with dyehouse vessel capacities requires calculating dry mass yields and vessel fill limits to prevent shade variation.
Dye lot conversion schedule reconciliation requires matching greige bulk density and nozzle hydraulics to vessel capacity, preventing pump cavitation and shade drift.
Long term greige storage transfers financial risk from yarn pricing to wet processing variance, requiring strict storage controls and clear dyehouse testing bounds.
Split dyeing batch shade consistency depends on spectrophotometric reflectance curve matching across multiple illuminants and strict stenter thermal control.
Enforce CIE DE2000 spectrophotometric shade tolerance limits under dual illuminants with strict fabric conditioning to prevent batch rejections.
Reconciling master greige orders across multi-tube jet vessels requires matching greige linear mass to individual tube capacities while maintaining fixed liquor ratios across all operational runs.
Dynamic control of ambient regain, pad bowl deflection, wet-bulb drying temperatures, and steam saturation halts continuous shade drift across variable weather.
Equalizing parallel nozzle pressure across multi-tube jet vessels eliminates inter-chamber shade variations by balancing rope speed and liquor turnover.
Dynamic psychrometric compensation continuously balances evaporation and pickup in pad boxes, preventing dyestuff molarity drift and head-to-tail shade defects.
Matching intermediate infrared radiant emission wavelength to polyelectrolyte thermal gelation viscosity prevents dye migration in continuous wet processing.
Dense cellulosic wet transport is limited by swelling-induced micro-pore collapse; forced hydraulic convection and controlled diffusion times prevent core pale-outs.
Spectrophotometric color tolerancing requires D65 optical calibration, CIEDE2000 ellipsoidal metrics, and strict substrate backing to ensure bulk dye batch agreement.
Uncontrolled greige storage triggers moisture migration, lipid autoxidation, and sizing retrogradation, which impair surface wettability and cause severe dye absorption variances.
Controlling multi-mill spectral reflectance variance requires standardized d/8° geometry, digital CxF3 master distribution, and strict CIEDE2000 tolerances.
Commission dyeing defect liability requires contractual tripartite agreements, pre-process greige verification gates, and analytical fault isolation.
Heavy cotton duck dyeing requires progressive electrolyte dosing, high-pressure liquor penetration, and strict tension control to eliminate surface ring-dyeing.
Dynamic hydraulic header balancing and nitrogen expansion tank padding prevent nozzle cavitation and rope speed divergence during fast vessel thermal ramps.
CIEDE2000 tolerances below 0.8 dE00 prevent visual metameric mismatches between garment shells and trims under D65 and retail LED illuminants.
Matching digital ink shear viscosity with controlled pad pick-up targets optimizes optical density and suppresses edge bleeding in high-speed printing.
High-speed pad dyeing liquor control requires ultra-low volume troughs and closed-loop radar dosing to eliminate tailing and shade drift across bulk runs.
Relative humidity drops accelerate solvent evaporation in heated pad troughs, concentrating liquor and causing head-to-tail shade drift in continuous dyeing.
Mechanical volumetric dosing calibration requires precise stroke volume verification, backpressure simulation, and fluid density compensation to eliminate shade tailing and maintain bulk color consistency across continuous dyeing lines.
Real-time conductivity-controlled electrolyte dosing stabilizes dye uptake on variable greige duck by throttling salt delivery to match fiber wetting rates.
Digital color measurement relies on standardized optical geometry, CIEDE2000 metrics, and controlled conditioning to prevent bulk shade rejections.
Implementing CIEDE2000 with 2:1:1 parametric weighting on continuous dye lines eliminates corner sorting errors and halves false rejects on textured goods.
Restricting vessel volume below fifteen litres ensures complete bath turnover within three minutes, stopping reactive dye hydrolysis and knit loop distortion.
Metamerism index limits below 0.5 under secondary retail illuminants prevent shade rejection and dyestuff rework across global fabric supply chains.
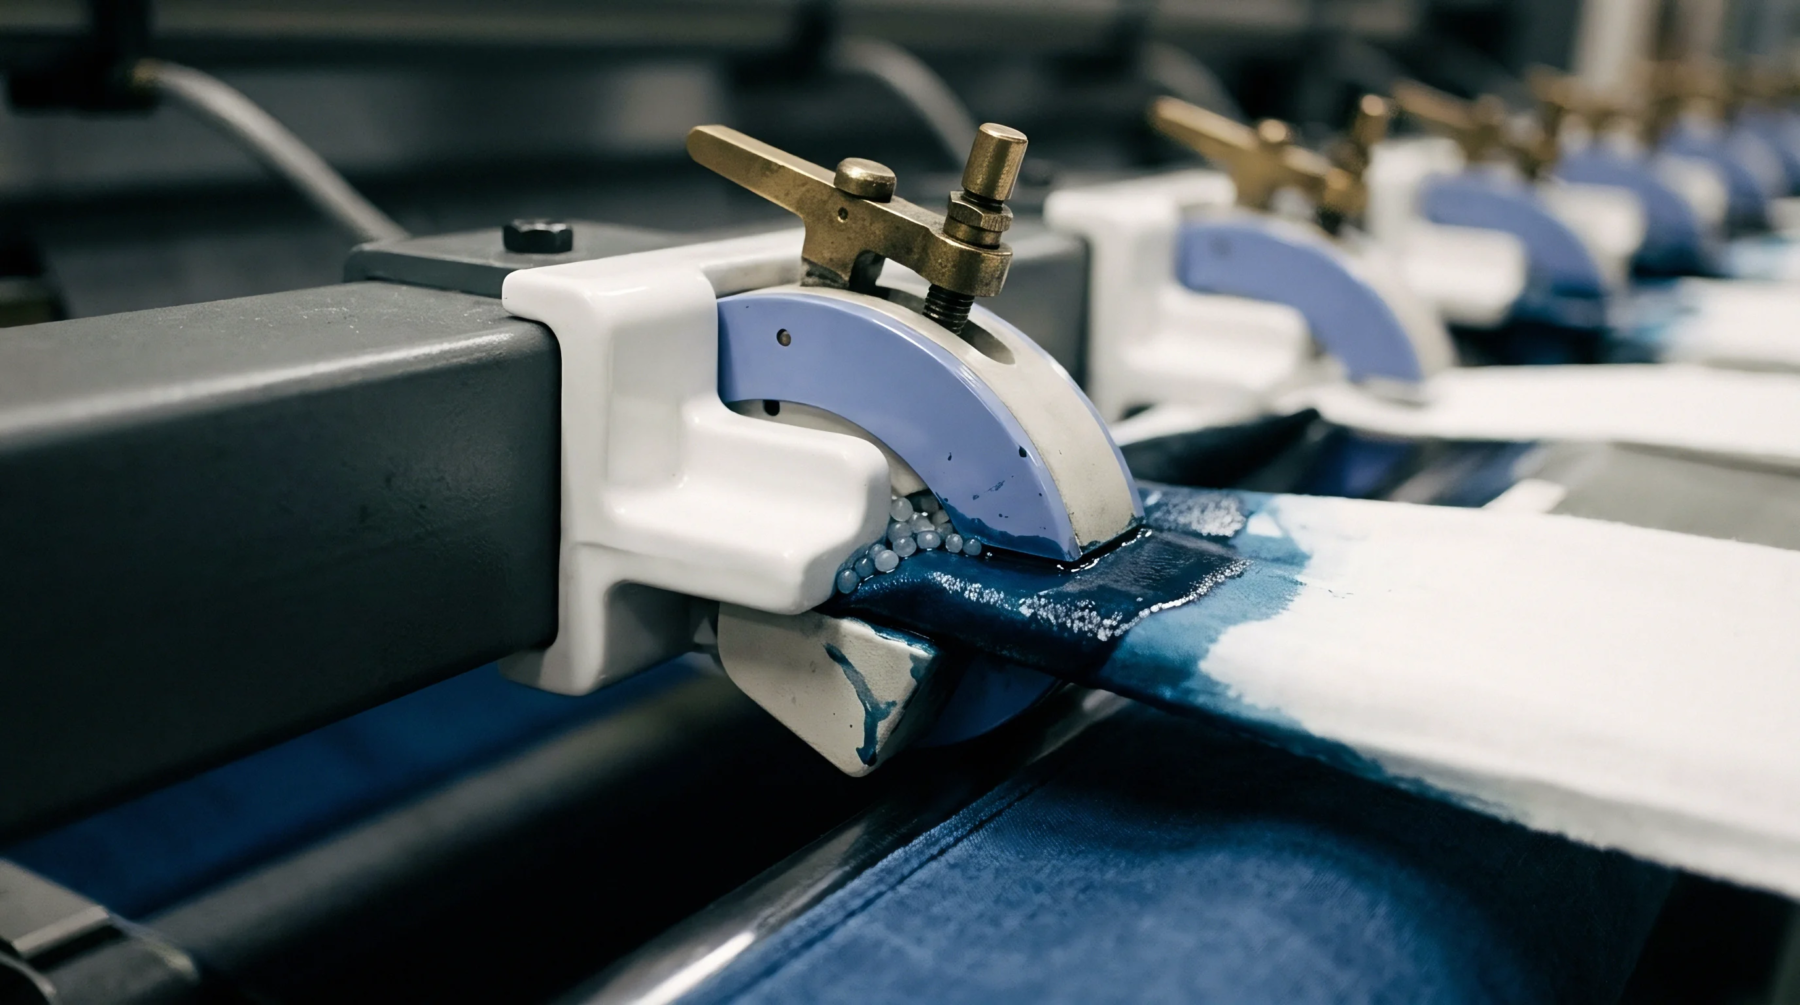
Spatial non-uniformity stems from roll deflection, drying airflow gradients, and thermal drift, requiring multi-point spectrophotometry to enforce debit remedies.
Secondary metamerism under store fluorescents is controlled by constraining dye reflectance crossover spikes to keep the index below 0.5 Delta E.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.