Fabric Weight Tolerance Written as a Range the Mill Holds
Fabric weight tolerance written as a mill range holds commercial validity only when tested under ISO 139 standard atmosphere using ISO 3801 methods.
Fabric weight tolerance written as a mill range holds commercial validity only when tested under ISO 139 standard atmosphere using ISO 3801 methods.
Type approval certificates prove mill capability, while targeted lot indicator testing on repeat orders verifies shipment conformity before vessel loading.
Harmonize multi-market physical fabric testing by implementing worst-case envelope protocols and validating ISO 17025 laboratory accreditation scopes.
Correlating loom sett and machine gauge to wet shrinkage requires matching grey thread density and stitch length to wet relaxation limits before finishing.
Modeling long-term stress relaxation thresholds in core-spun jet processed elastic fabrics requires balancing spinning core draft with stenter heat setting to prevent interfacial shear slip and retractive decay.
Optimize air-jet polyurethane wovens by setting stenters to 190°C with +24% overfeed, holding heat setting efficiency above 88% and growth below 2.5%.
Crosslink density decay during repeated wet processing dictates the trade-off between durable crease recovery and catastrophic fabric tear strength loss.
Geometrical modeling of crimp interchange predicts width collapse during wet finishing by balancing yarn swelling against mechanical jamming boundaries.
Textile qualification requires mapping baseline chemical limits and physical standards to accredited lot-level test reports before releasing purchase orders.
Commission dyeing defect liability requires contractual tripartite agreements, pre-process greige verification gates, and analytical fault isolation.
Calibrate stenter line speed to effective core dwell time above 190°C rather than total chamber residence to prevent spandex degradation and knit shrinkage.
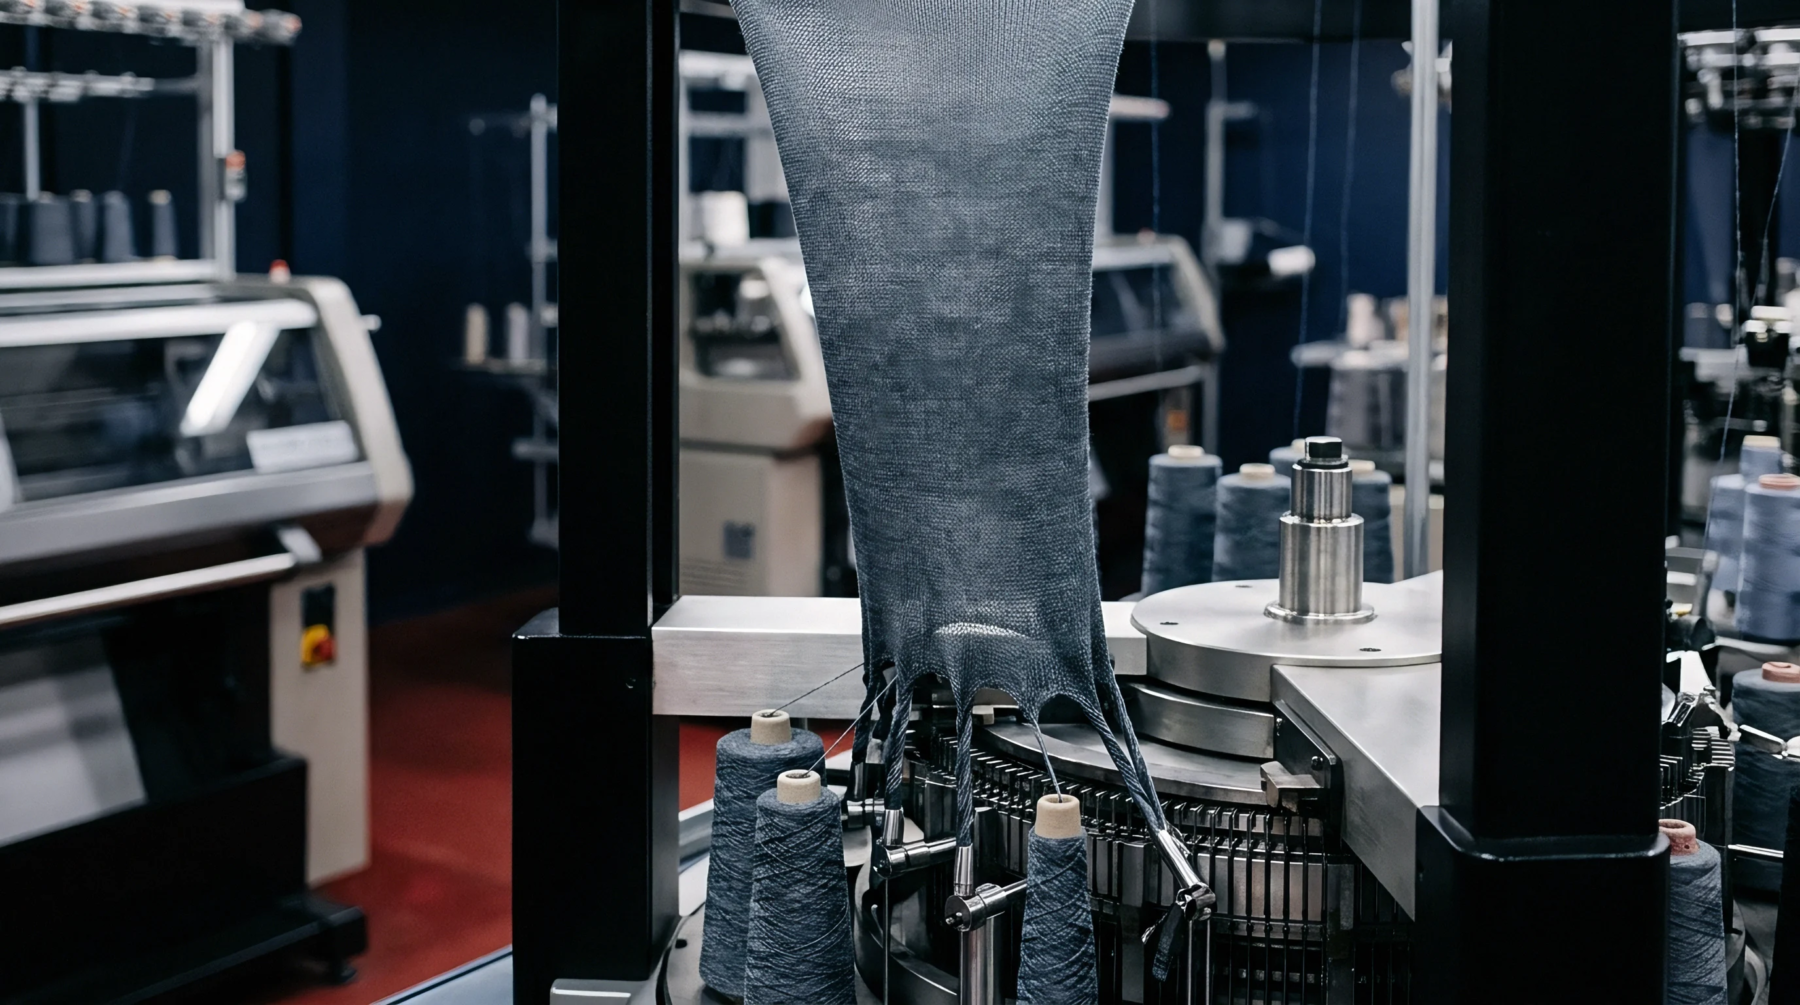
Matching knitting machine gauge to yarn linear density fixes loop tightness factor, setting the upper limit for aqueous dimensional contraction during wet finishing.
Symmetric nozzle velocity between 18 and 22 m/s during intermediate drying prevents dye migration and maintains shade uniformity in polyester cotton blends.
Continuous stenter overfeed forces must balance longitudinal yarn buckling thresholds against friction to set finished course density without cloth corrugation.
Biaxial thermal stenter extension alters yarn crimp balance through coupled viscoelastic relaxation and Peirce geometry shifts, dictating final fabric dimensional stability.
Derive loom reed width by compounding greige take-up and wet finishing contraction percentages onto target cuttable width while balancing dent air space ratios.
Warp and weft crimp exchange in high-density weaving shifts structural waviness across processing, dictating finished sett, shrinkage, and air permeability.
Predicting plain weave jamming limits prevents fabric distortion and secures dimensional stability across caustic mercerizing, dyeing, and wash finishing.
Quantifying greige crimp exchange and jamming limits prevents beat-up fabric defects, off-loom width loss, and incorrect finished weight calculations.
Synchronize multi-motor continuous dye drives to maintain warp tension under 1.8 N/cm, preventing twill skew, pick count loss, and face-to-back shading.
Controlled stenter dwell at 185-195°C stabilizes polyurethane hard segments to minimize viscoelastic force decay and garment bagging in stretch wovens.
Stabilizing hard segment crystallization via controlled thermal quenching and stenter dwell times eliminates elastomeric creep and width variation in stretch goods.
Specify conditioned mass under ISO 3801 and minimum cuttable width excluding selvedges to lock in garment yield and protect unit production economics.
Warp cover factor quantifies yarn area coverage using thread density and yarn diameter equations to control fabric porosity, mechanical strength, and production speed.
Contractual action limits combine guarded acceptance rules and split-sample referee protocols to arbitrate repeat textile test variations fairly.
Fine gauge knit contraction relies on balancing hydrodynamic wet relaxation with stenter overfeed to lock loop geometry before garment cutting.
Predictive crimp exchange modeling calculates yarn path geometry shifts between weaving and finishing to secure finished pick count, yield, and width.
Finite element modeling reveals hydrothermal yarn strain in jet dyeing stems from drag forces exceeding wet elastic limits near polymer glass transition.
Predictive modeling of inter-yarn friction decay under steam enables precise line overfeed synchronization to lock finished dimensional stability and yield.
Verify woven fabric density on conditioned finished goods using ASTM D3775 or ISO 7211-2 to catch off-loom overfeed tricks and protect garment seam strength.
Expertise is a utility, not a secret. sentiention™ publishes its working knowledge as open reference: intelligence layer covering the materials it sources, the markets it enters, and the reference that serves both.